
High-Pressure Beam Rail Edge Banding Machine
A heavy beam on a steel rail holds the door blank flat, a double-stack disc trims the band top and bottom, and the 35° ends back off before they chip a corner.
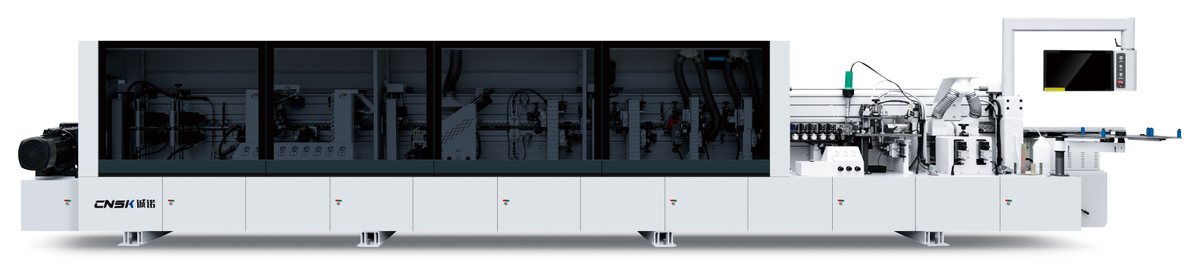
Overview
- Sixteen cells in the order printed on the sheet: 21.5-inch industrial computer, high-pressure beam on a heavy steel rail, separating agent, pre-milling, heat lamp, two-colour PUR no-cleaning pot, swing-type pressing, double-stack disc trimming, scraping 1, scraping 2, hinged flat scraping, 35° end and tail trimming, four-head tracking, cleaning, polishing 1 and polishing 2.
- The beam is a custom heavy section on a heavy steel rail: the load of a 60 mm door blank is carried by the rail rather than by the panel.
- A two-colour PUR no-cleaning pot sits at station 06, and the heat lamp in front of it pre-heats the board and the glue.
- Panels from 40 mm wide and 8 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on a 9,280 mm frame, 950 mm wide and 1,800 mm high, with 22 kW installed.
- The laser unit and its cooling head are optional on this frame: the sixteen cells above are the standard build, and the laser pair is quoted in addition.
- Both scraping heads and the hinged flat scraper run ahead of the two polishing heads, so the edge comes off the line flat rather than merely trimmed.
Station sequence
Station 01 is the 21.5-inch computer and station 02 the high-pressure beam on its steel rail; the sixteen cells follow the order printed on the sheet. The sheet numbers the two scraping heads and the two polishing heads ① and ②, written here as 1 and 2.
Technical data
| Model | CN300 |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 8 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Heavy-duty high-pressure beam, electric lift |
| Processing stations | 16 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 22 kW |
| Machine size (L × W × H) | 9280 × 950 × 1800 mm |
Values from the CN300 technical data sheet in the 2026 configuration list. That sheet lists the laser operating system and its cooling unit as optional cells on this frame; the sixteen stations on this page are the standard build.
What the machine is built to do
- High-pressure beam on a railThe beam is a custom heavy section carried on a heavy steel rail, so the panel is held flat while the band is pressed.
- Two-colour PUR potThe no-cleaning pot switches between two adhesive colours without a solvent flush.
- Double-stack disc trimmingTwo stacked discs trim the band top and bottom in one pass, which is what keeps a 60 mm edge square.
- 35° end trimming with evasionThe end heads cut at 35° and back off automatically on a thicker board or band, so corners are not chipped.
- Hinged flat scrapingA hinged scraper follows the panel face and lifts surplus hot-melt off flat.
- Two polishing headsPolishing 1 and 2 finish the edge, so the joint reads even against a lacquered door.
More from the CN series
Servo Heavy-Duty Laser Edge Bander
Laser bonding with no glue line, on panels from 8 mm and strips down to 40 mm.
Automatic edge banding machine
Seventeen cells with two heat lamps, two glue stations and two pressing groups, servo fine trimming, 26.4 kW.
Servo Narrow Edge Automatic Edge Bander
Fourteen cells for narrow stock from 40 mm: EVA furnace, fast-melt tank, servo fine trimming, four-head tracking.
Put CN300 against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.