
Intelligent Automatic Edge Sealing Machine
The belt build is the one to specify when the bander sits behind a saw: the panel arrives on the track conveyor and the same sixteen cells finish the edge without a hand-fed table in front.
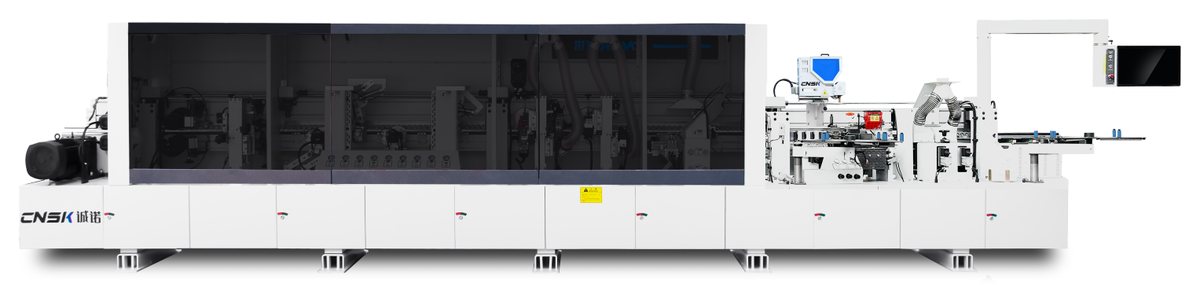
Overview
- Sixteen cells in the order printed on the sheet: track conveyor, high-definition wide screen, separating agent, pre-milling, heat lamp, glue pot, fast-melt tank, servo tape feed, head-and-tail trimming, rough trimming, servo fine trimming, four-head tracking, scraping, precise flat scraping, cleaning and polishing.
- Panels from 50 mm wide and 9 to 60 mm thick, with band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on an 8,100 mm frame, 800 mm wide and 1,900 mm high, with 18 kW installed.
- The EVA pot carries a fast-melt tank, so the adhesive reaches working temperature in less time and the first panel of a shift is not scrap.
- Servo tape feed sets the band length from the screen rather than from a hand-set stop, which matters on short runs.
- Four-head tracking runs the corners, then scraping and precise flat scraping take the surplus off the panel face before the polishing head.
- The pressure beam lifts electrically, and the recipe list sits on the wide screen instead of on a row of dials.
Station sequence
Station 01 is the track conveyor and station 02 the wide screen; the sixteen cells then run from separating agent to polishing in the order printed on the sheet.
Technical data
| Model | CN810D(Belt) |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 50 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 16 |
| Control screen | High-definition wide screen |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 18 kW |
| Machine size (L × W × H) | 8100 × 800 × 1900 mm |
Values from the CN810D technical data sheet in the 2026 configuration list. The model is printed there as CN810D(Belt), and the page keeps that as written.
What the machine is built to do
- Belt infeedThe model is listed as CN810D(Belt) on the data sheet. That build takes the panel from a conveyor line, which is the version to ask for when the bander works behind a panel saw rather than as a stand-alone cell.
- Fast-melt tank on the potA second tank brings the melt up to working temperature while the pot holds it there, so a cold start costs minutes rather than a shift.
- Servo tape feedBand length is a screen value, and the feed repeats it panel after panel without an operator checking a mechanical stop.
- Four-head trackingThe tracking unit carries four motors, so both ends of the band turn the corner in one pass instead of being cut square across it.
- Double scrapingScraping runs on both faces of the edge, then the flexible scraper takes the surplus hot-melt off the panel surface.
- Eight metre frame8,100 mm long and 800 mm wide: a compact line that still carries pre-milling, two glue functions and polishing.
Other formats
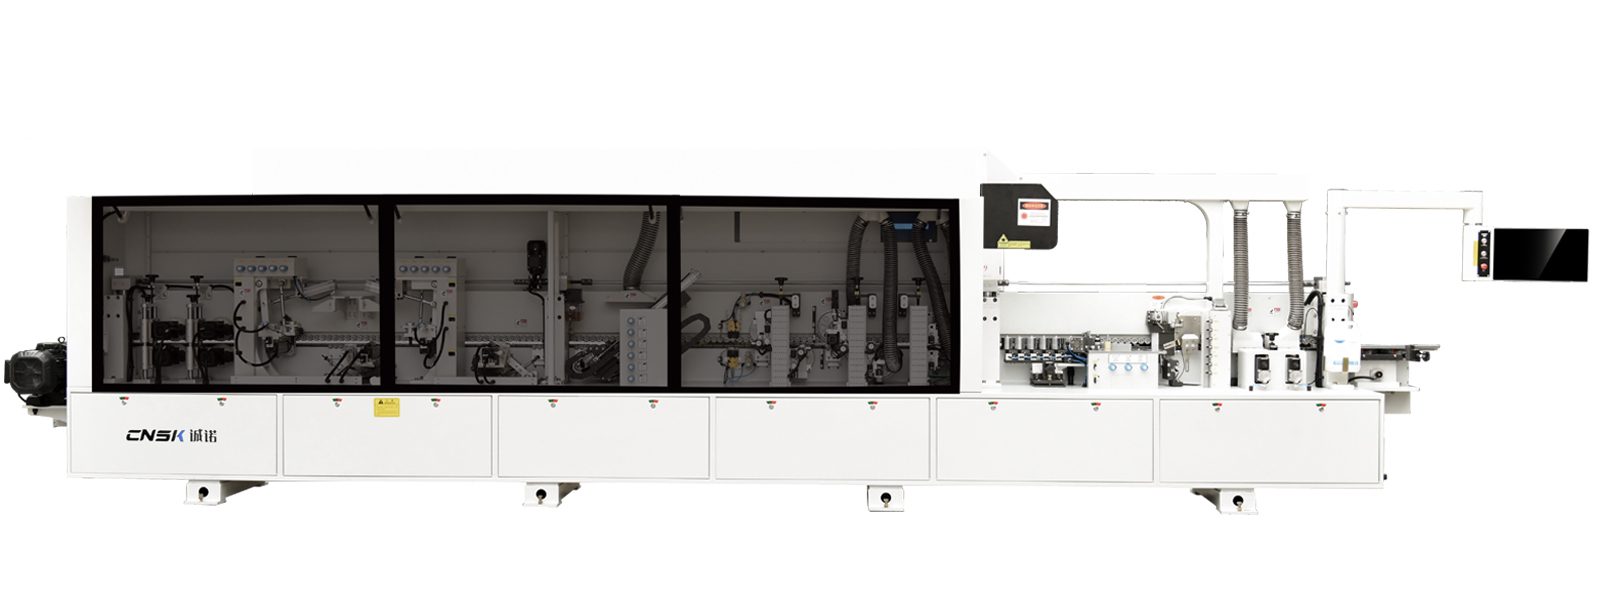
Servo Heavy-Duty Laser Edge Bander
Laser bonding with no glue line, on panels from 8 mm and strips down to 40 mm.
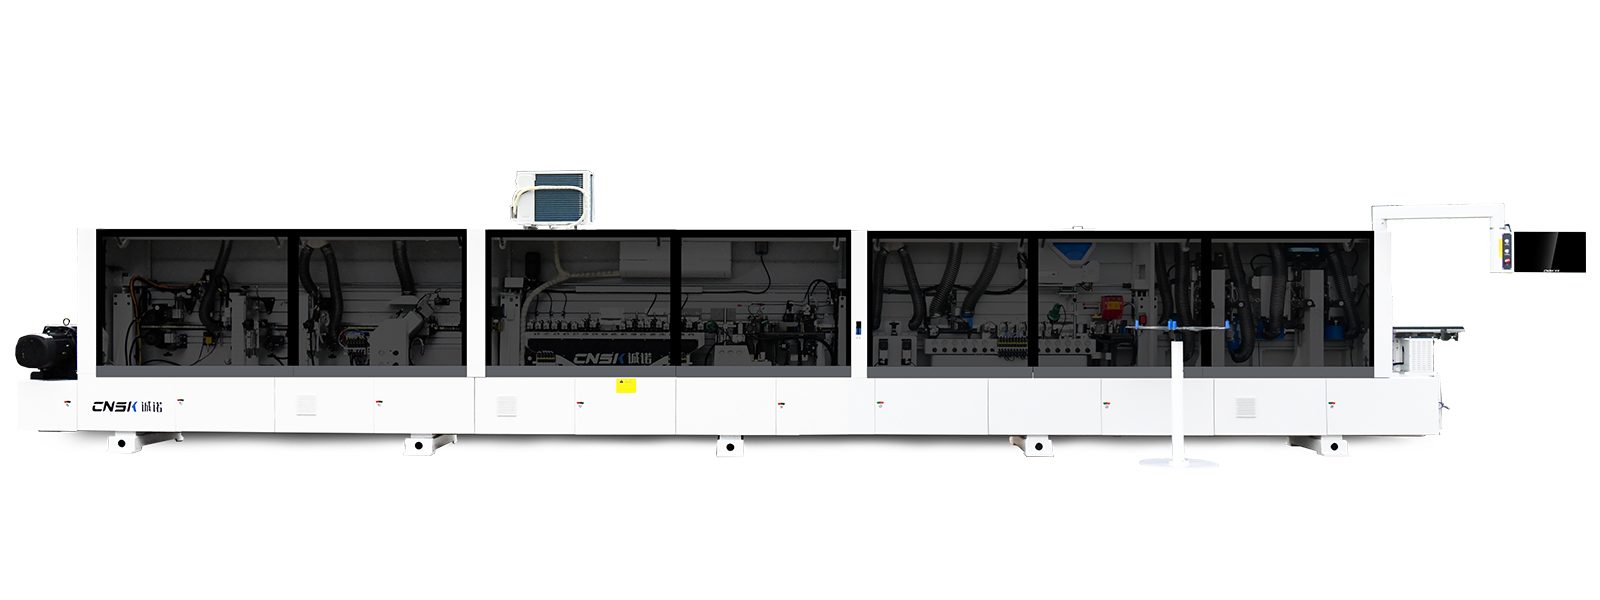
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
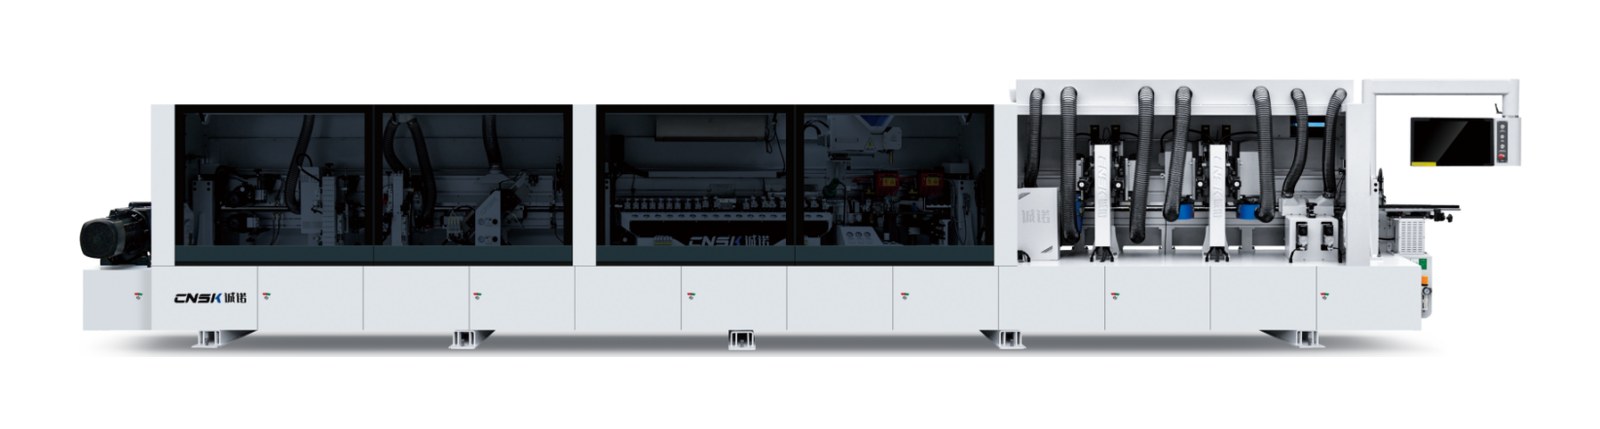
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
Put CN810D(Belt) against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.