
Automatic edge banding machine
Two glue stations, each with its own heat lamp and pressing group: the second application is heated and pressed again, so a band that has already cooled is not pressed cold.
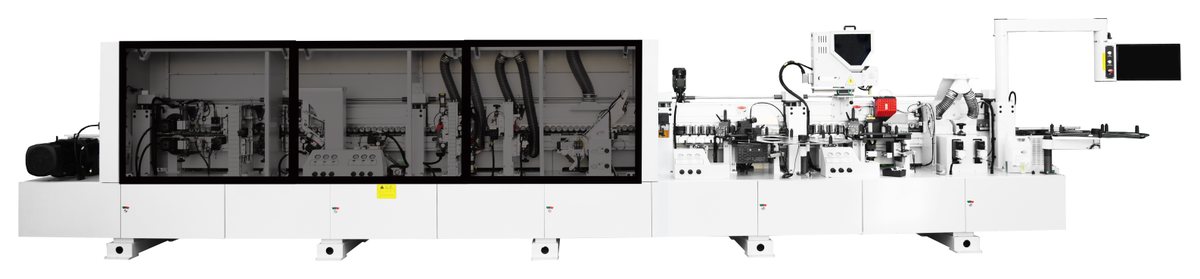
Overview
- Seventeen cells in the order printed on the sheet: wide screen, separating agent, pre-milling, heat lamp 1, glue station 1, pressing group 1, heat lamp 2, glue station 2, pressing group 2, head-and-tail trimming, rough and servo fine trimming, head tracking, servo scraping, flexible flat scraping, cleaning, polishing head 1 and polishing head 2.
- Panels from 50 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on an 8,700 mm frame, 850 mm wide and 1,700 mm high, with 26.4 kW installed.
- Rough trimming and servo fine trimming share one unit, so the band is not re-clamped between the two cuts.
- Head tracking runs two high-speed motors and turns the band round the corner before the scraping heads
- Servo scraping is followed by a flexible flat scraper, which follows the panel face instead of cutting to a fixed depth.
- Two polishing heads finish the edge, which is the step that decides how the band reads against a lacquered door.
Station sequence
Station 01 is the wide screen; the seventeen cells then run from separating agent to the second polishing head in the order printed on the sheet.
Technical data
| Model | CN860D |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 50 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 17 |
| Control screen | High-definition wide screen |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 26.4 kW |
| Machine size (L × W × H) | 8700 × 850 × 1700 mm |
Values from the CN860D technical data sheet in the 2026 configuration list.
What the machine is built to do
- Two glue applicationsHeat, glue, press, heat, glue, press: the second application is made on a warm band rather than a cold one, which is what a thick or veneer band needs.
- Two polishing headsThe second pair of cotton wheels follows the first, for a higher sheen than a single head gives.
- Servo fine trimmingThe fine head is positioned by servo, so the depth is a screen value and it repeats after a band change.
- Head trackingTwo high-speed motors carry the tracking head, so the corners of a thin band are turned rather than cut square.
- Flexible flat scrapingA sprung scraper follows the panel face on thin boards, where a fixed-depth scraper would mark the surface.
- 8.7 m frame850 mm wide and 1,700 mm high: a straight-line machine that fits a bay without a pit.
More from the CN series
Servo Heavy-Duty Laser Edge Bander
Laser bonding with no glue line, on panels from 8 mm and strips down to 40 mm.
Servo Narrow Edge Automatic Edge Bander
Fourteen cells for narrow stock from 40 mm: EVA furnace, fast-melt tank, servo fine trimming, four-head tracking.
High-Pressure Beam Rail Edge Banding Machine
Sixteen cells on a high-pressure beam rail: PUR pot, disc trimming, 35° end trimming and two polishing heads, 22 kW.
Put CN860D against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.