
45° Bevel and Straight Edge Bander, EVA
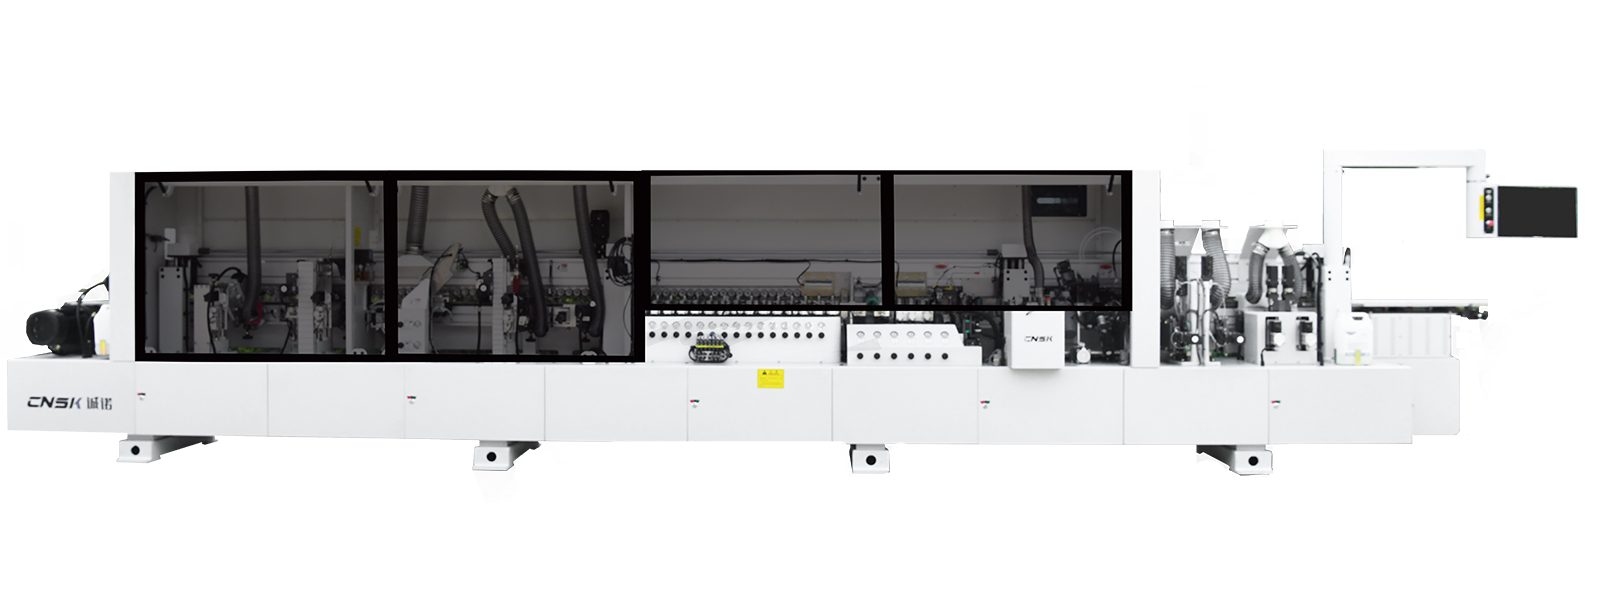
A handle-free groove and a 45° bevel on the same bed, with the band cut on both faces and pressed through the profile: the order that normally needs two machines runs on one, with the EVA furnace on the frame.
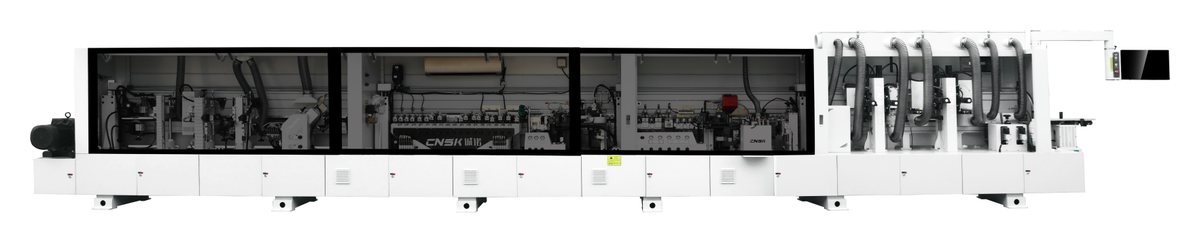
Overview
- Twenty-five numbered cells: 21.5-inch industrial computer, separating agent, pre-milling, servo forming cutter 1/2, servo forming cutter 3/4, bottom chamfer, bevel edge gluing, edge band grooving, straight edge gluing, feeding unit, bevel and straight synchronous pressing, panel with handle-free groove and band gluing, EVA gluing furnace, transmission pressing, heat gun, baking lamps 1 to 4, seventeen-group servo forming and pressing, rough trimming, four-speed dual-track head-and-tail trimming, fine trimming, scraping, notch trimming, second scraping, cleaning and servo polishing.
- Both formats on one line: a separate bevel gluing unit and a separate straight edge gluing unit, then a pressing section that loads the bevel and the straight face together.
- The handle-free groove is glued in the same station that glues the panel face and the band itself, so the wrap is bonded along its whole width instead of at the edges only.
- Two servo cutter pairs mill the profile on both faces of the band; bottom chamfer then sets the lower edge to the notch contour so the band folds under the panel.
- 11,620 mm frame, 1,150 mm wide, 1,900 mm high, 67 kW, 8 m/min: the largest build in the handle-free range.
- Panels from 120 mm wide; 18 to 22 mm thick with 55 to 60 mm band on the handle-free profile, 9 to 25 mm thick with 30 to 40 mm band on the bevel and straight format.
- Fine trimming, scraping, notch trimming, a second scraping head, cleaning and servo polishing close the sequence, with the polish head following the profiled contour.
Station sequence
Station 01 is the 21.5-inch industrial computer; twenty-five numbered cells run from separating agent to servo polishing, with the EVA furnace at station 13 and the bevel and straight gluing units at stations 07 and 09.
Technical data
| Model | FM756JCX |
| Feed rate | 8 m/min |
| Panel width | ≥ 120 mm |
| Panel thickness | 18 – 22 mm (handle-free) / 9 – 25 mm (bevel and straight) |
| Edge band thickness | 0.55 – 0.6 mm (handle-free) / 0.8 – 1.0 mm (bevel and straight) |
| Edge band width | 55 – 60 mm (handle-free) / 30 – 40 mm (bevel and straight) |
| Pressure beam | Electric lift |
| Processing stations | 25 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 67 kW |
| Machine size (L × W × H) | 11620 × 1150 × 1900 mm |
Values from the FM756JCX technical data sheet in the 2026 configuration list. The sheet prints the thickness, band thickness and band width in two columns, one for the handle-free profile and one for the bevel and straight format, and they are shown here in the same order. The glue on this build is EVA, melted in the furnace that sits at station 13; the sheet also lists the bevel and straight gluing units at stations 07 and 09 as EVA pots. The same frame is built with an external two-colour PUR pot instead, and that variant has its own page.
What the machine is built to do
- Two formats, one bedHandle-free profile and 45° bevel straight edge are both cut here: the format is a recipe, not a second machine and a second operator.
- Bevel and straight gluing kept apartTwo gluing units, one for the bevel band and one for the straight edge, each with its own setting instead of a shared nozzle.
- Synchronous pressingThe bevel and the straight face are pressed in the same pass, so neither is run at the pressure of the other.
- Handle-free groove glued in linePanel face, groove and band are glued at one station, which is what holds a wrap that reaches round the groove.
- Seventeen forming groupsThe band is loaded along the whole profile until the shape sets, so a tight radius does not need a hand touch-up.
- EVA furnace buildThis page covers the EVA order; the same frame is also built with an external PUR pot, and that variant has its own page.
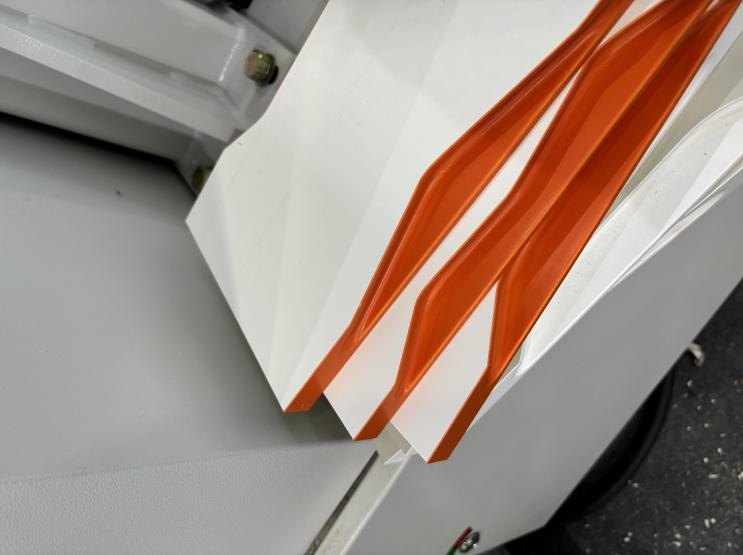
Edge samples
More from the 7 series
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
Five-Profile Arc and Bevel Edge Bander
Half-round, quarter-round, 45° bevel-straight, full bevel and duck-bill — five profiles on one bed.
Put FM756JCX against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.