
Soft-Forming Edge Bander with PUR
A wrap is cut at the notch as well as along the band: this line trims the notch before the press and again after it, which is where a soft-formed profile usually reads badly.
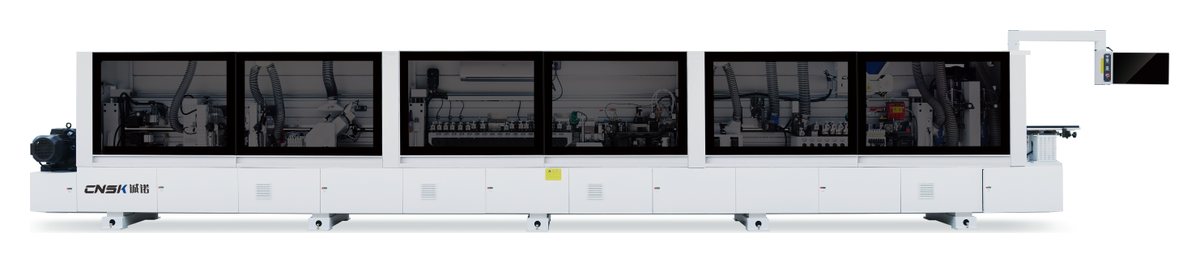
Overview
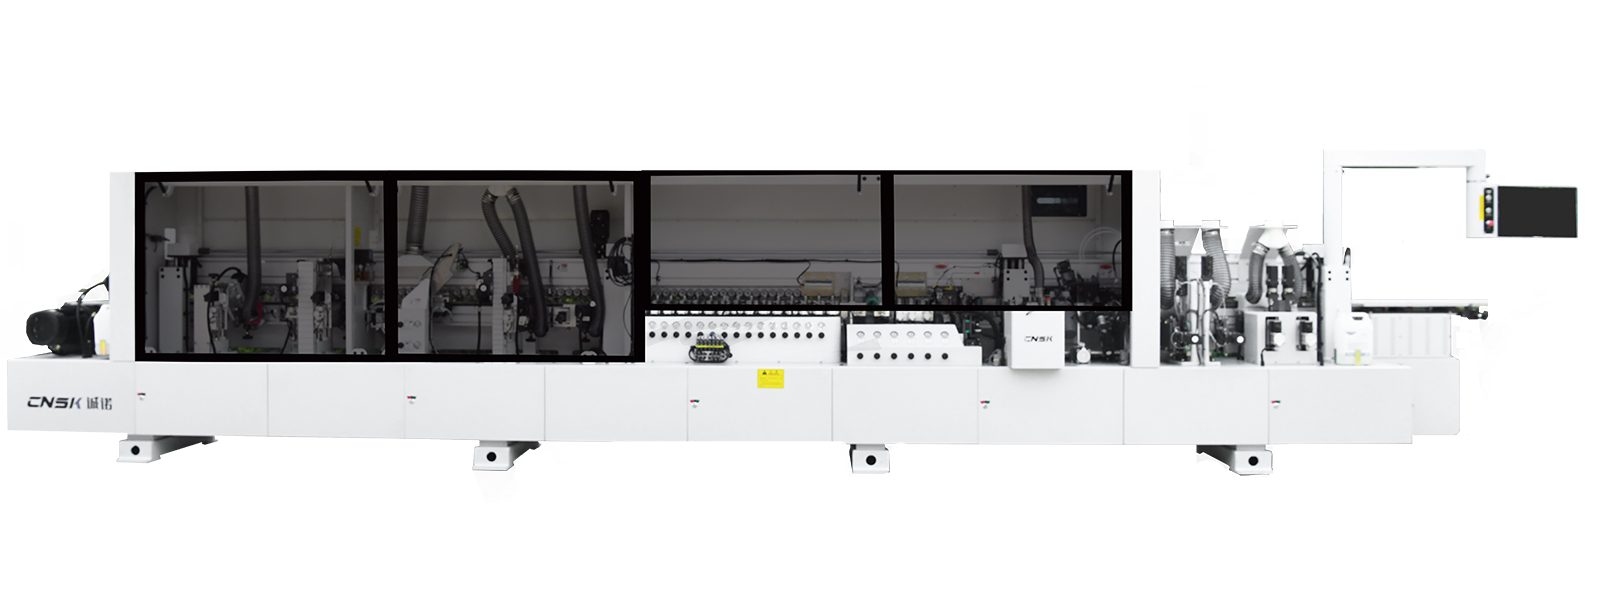
- Twenty-three numbered cells: 21.5-inch industrial computer, separating agent, servo forming cutter 1/2, gluing furnace, fast-melt glue, forming and pressing 1, notch trimming, rough trimming 1, pre-milling, panel preheating, two-colour PUR no-cleaning pot, heat gun, servo tape feed with notch and band gluing, transmission pressing, baking lamps 1 to 4, seventeen-group servo forming and pressing, rough trimming 2, four-speed dual-track head-and-tail trimming, fine trimming, scraping, notch trimming, cleaning and servo polishing.
- The station order follows the data sheet as printed: the forming press and the first notch trim sit before pre-milling, which is the sequence of this build rather than of the longer FM759JCS line.
- Notch trimming appears twice, once ahead of the rough trim and once behind scraping: the first cut opens the notch, the second takes the edge back to the panel face after the band has been pressed.
- EVA furnace with a fast-melt tank and a two-colour PUR pot on the same frame, and a heat gun before the servo tape feed.
- 10,800 mm frame, 950 mm wide, 1,850 mm high, 40 kW, 4,600 kg, at a single 7 m/min feed.
- Panels from 120 mm wide and 18 to 25 mm thick, band 0.5 to 0.7 mm thick and 30 to 65 mm wide.
- Seventeen servo forming groups hold the band along the profile; four baking lamps keep it soft from the tape feed to the press.
Station sequence
Station 01 is the 21.5-inch industrial computer; twenty-three numbered cells run from separating agent to servo polishing. The order is the soft-forming sequence printed on the sheet, not the straight-line sequence: the first notch trim sits at station 07 after the first forming press, pre-milling at station 09, and the second rough trim and the second notch trim close the forming section at stations 17 and 21.
Technical data
| Model | FM758JC |
| Feed rate | 7 m/min |
| Panel width | ≥ 120 mm |
| Panel thickness | 18 – 25 mm |
| Edge band thickness | 0.5 – 0.7 mm |
| Edge band width | 30 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 23 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 40 kW |
| Machine size (L × W × H) | 10800 × 950 × 1850 mm |
Values from the FM758JC technical data sheet in the 2026 configuration list. The sheet also gives the edge type as special-shaped and the machine weight as 4,600 kg. The station order is reproduced as printed on the sheet.
What the machine is built to do
- Notch trimming on both sides of the pressThe notch is opened before the forming section and finished after scraping, which is what keeps a soft-formed profile clean at the notch.
- PUR and EVA on one frameThe no-cleaning two-colour pot and the EVA furnace with a fast-melt tank are both fitted, so the adhesive follows the order.
- Seventeen forming groupsPressure is held along the whole profile, so a wrap closes without a second pass.
- Four baking lamps and a heat gunThe band stays soft across the forming section, so a tight radius folds without a white stress line.
- Servo tape feedTape feed is matched to the panel speed, and glue is applied in the notch and on the band at separate points.
- 7 m/min, 4,600 kgA heavy frame run slowly: a soft-formed band needs time under the lamps and under the press.
Edge samples
More from the 7 series
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
Five-Profile Arc and Bevel Edge Bander
Half-round, quarter-round, 45° bevel-straight, full bevel and duck-bill — five profiles on one bed.
Put FM758JC against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.