
High Pressure Beam Track Type Edge Bander
A high-pressure beam on a track: the beam holds the panel flat while two heated pressing groups put the band on, which is what a door blank needs before the trimmers reach it.
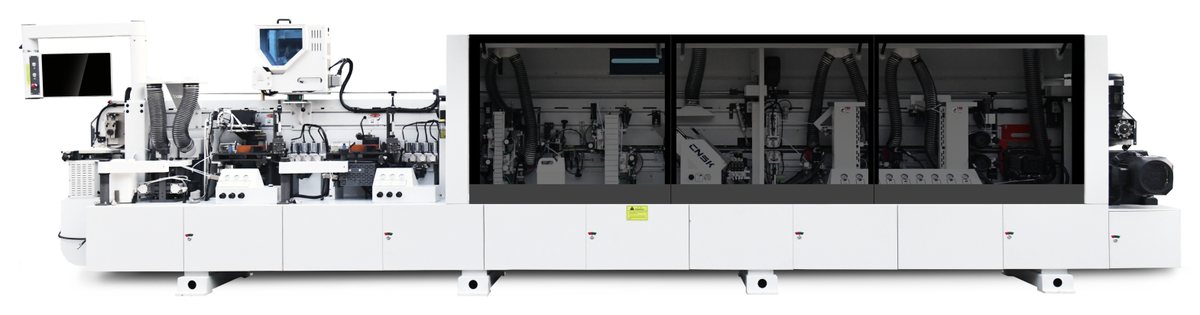
Overview
- Twenty-one cells in the order printed on the sheet: synchronous caterpillar conveyor, heavy-duty pressure beam, wide screen, separating agent, pre-milling, heat lamp, electric glue pot, heated pressing group 1, fast-melt tank, glue applicator, heated pressing group 2, servo fine trimming, unpowered trimming, servo scraping, head-and-tail trimming, flexible flat scraping, four-head tracking, cleaning, polishing, horizontal and vertical grooving and the track synchronous motor.
- Two glue applications, each followed by a heated pressing group, so the band is pressed warm twice rather than once cold.
- Panels from 60 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on a 7,960 mm frame, 950 mm wide and 1,900 mm high, with 28.95 kW installed and a body weight of 3,400 kg.
- Servo fine trimming and servo scraping are positioned from the screen, so the depth repeats after a band change.
- Four-head tracking runs the corners before cleaning and the single polishing head.
- A horizontal and vertical grooving unit at station 20 lets the line also produce groove profiles.
Station sequence
Station 01 is the synchronous caterpillar conveyor and station 02 the pressure beam; the twenty-one cells follow the order printed on the sheet, with the second heated pressing group at station 11.
Technical data
| Model | FMK850A |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 60 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Heavy-duty electrical lift, high-pressure beam on a track |
| Processing stations | 21 |
| Control screen | High-definition wide screen |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 28.95 kW |
| Machine size (L × W × H) | 7960 × 950 × 1900 mm |
Values from the FMK850A technical data sheet in the 2026 configuration list; the sheet also gives the transmission mode as synchronous track and the body weight as 3,400 kg.
What the machine is built to do
- High-pressure beam on a trackThe pressure beam runs on a track rather than a fixed bridge, so the panel is held flat across its full length before the glue stations.
- Heated pressing, twiceBoth pressing groups are heated: the band is brought back up to temperature at the joint instead of being pressed onto a cooling face.
- Electric glue pot with fast-meltAn electric pot holds the EVA melt and a fast-melt tank brings new granulate up to temperature, so a cold start does not cost a shift.
- Servo trimming and scrapingBoth heads are servo-positioned, which is what keeps the cut even along a 7.9 m run.
- Unpowered head where it helpsThe unpowered trimmer cuts without its own drive motor, so there is less to wear and less to clean.
- Grooving at the endStation 20 grooves horizontally or vertically, which is the difference between a bander and a bander that also makes groove profiles.
More from the FMK series
Intelligent laser crawler edge banding machine
Eighteen cells on a 10.3 m crawler bed: two-colour PUR pot, laser bonding, swing cutter and notching, 28 kW.
Intelligent PUR track edge banding machine
Reverse-layout PUR line, eighteen cells: two PUR pots with heat lamps, unpowered trimming and head tracking, 16 to 26 m/min at 28 kW.
HeavyDuty Laser TrackType Edge Banding Machine
Twenty cells on a synchronous track: two EVA furnaces, laser unit, servo trims and chamfer tracking, 36 kW.
Put FMK850A against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.