
Laser Edge Bander with PUR
A laser with no glue line, and a PUR pot on the same frame for the orders that still want an adhesive: the bond is chosen per batch, not per machine.
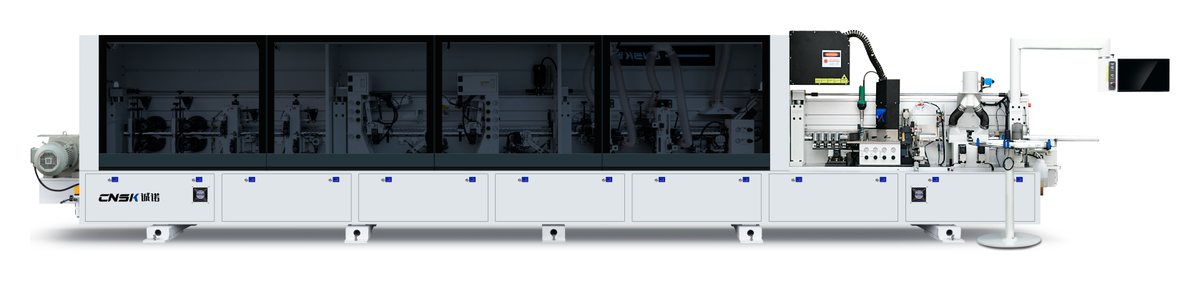
Overview
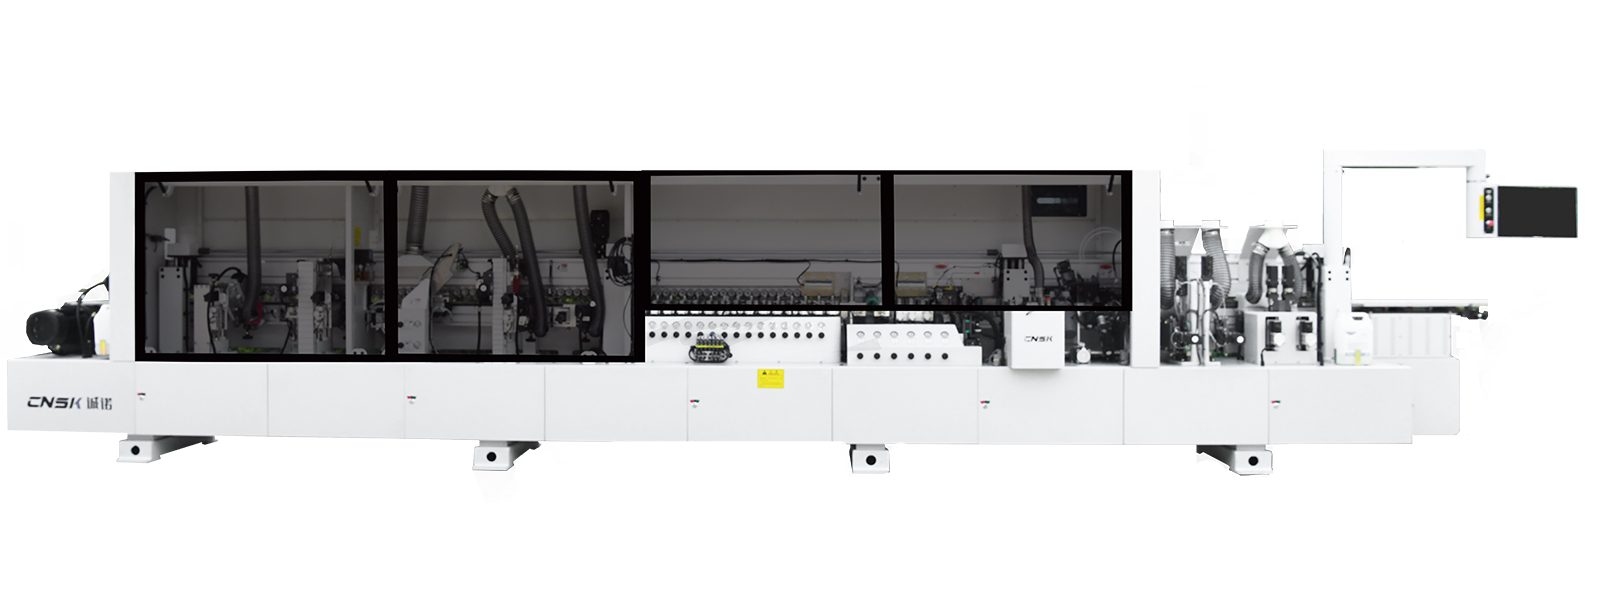
- Twelve numbered cells: 21.5-inch screen operation interface, pre-milling, two-colour PUR no-wash pot, laser device, servo-precision tape feed with yaw pressing, head-to-tail alignment, double trimming, four-head tracking, double scraping, cleaning, polishing and polishing.
- Laser bonding activates the functional layer on the band, so the joint closes without a glue line; the PUR pot is there for the orders where an adhesive is still specified.
- Servo-precision tape feed with yaw pressing: the pressing unit turns to the edge angle while the feed is matched to the panel speed, which is what keeps a band square on an inclined face.
- Head-to-tail alignment runs before double trimming, so both ends are cut to the same reference instead of one being set against the other.
- Four-head tracking rounds the corners at both ends, then double scraping cleans the band and the film before two polishing stations.
- 9,900 mm frame, 1,050 mm wide, 1,850 mm high, 23 kW, at 16 to 23 m/min.
- Panels from 40 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide: the narrow-panel geometry of the 708 family with a laser bond.
Station sequence
Station 01 is the 21.5-inch screen; twelve numbered cells run from pre-milling to the second polishing station.
Technical data
| Model | H760 |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 12 |
| Control screen | 21.5-inch screen operation interface |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 23 kW |
| Machine size (L × W × H) | 9900 × 1050 × 1850 mm |
Values from the H760 technical data sheet in the 2026 configuration list. The sheet prints the beam lift in Chinese characters; it is shown here as electric lift.
What the machine is built to do
- Laser bond, no glue lineThe functional layer on the band is activated by the laser and pressed onto the panel, so the joint reads as an edge, not as a glued edge.
- PUR available on the same frameA two-colour no-wash pot for the orders that still call for adhesive, switched in instead of run in place of the laser.
- Yaw pressingThe pressing unit yaws to the edge angle with the tape feed servo-matched, so the band sits square on an inclined face.
- Head-to-tail alignmentBoth ends are brought to one reference before the trim, which is what keeps a pair of panels the same length.
- Four-head tracking and double scrapingThe corners are tracked at both ends, and two scraping heads take the band and the film before polishing.
- 16 to 23 m/min on a 40 mm stripThe narrow-panel line at production speed, rather than a slow laser cell.
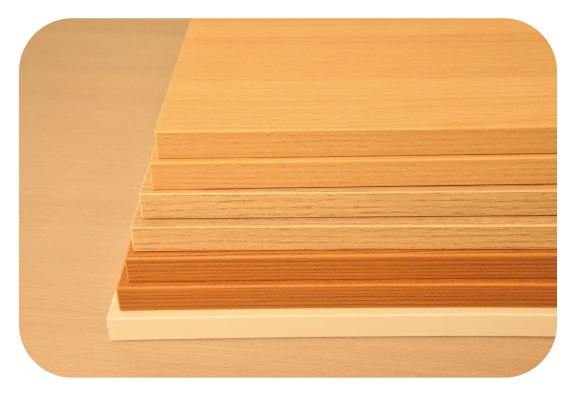
Edge samples
More from the 7 series
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
Five-Profile Arc and Bevel Edge Bander
Half-round, quarter-round, 45° bevel-straight, full bevel and duck-bill — five profiles on one bed.
Put H760 against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.