
Laser Edge Bander with Maglev Tracking
Both the end trim and the tracking head float on magnetic rails: at 42 m/min that is what keeps the corner round and the end square on the same panel.
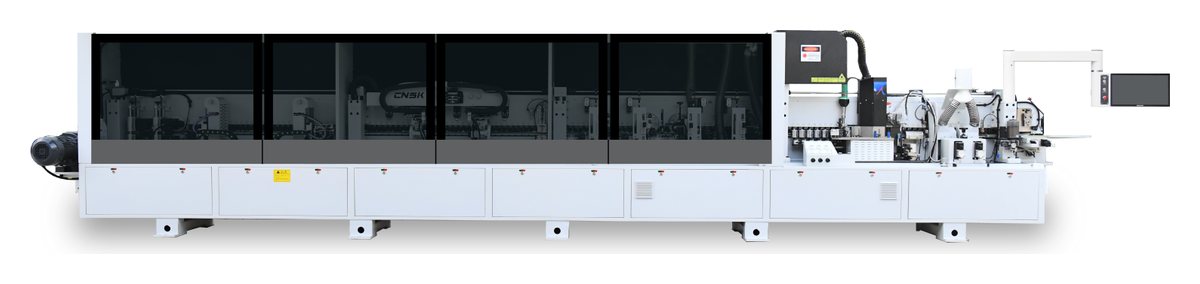
Overview
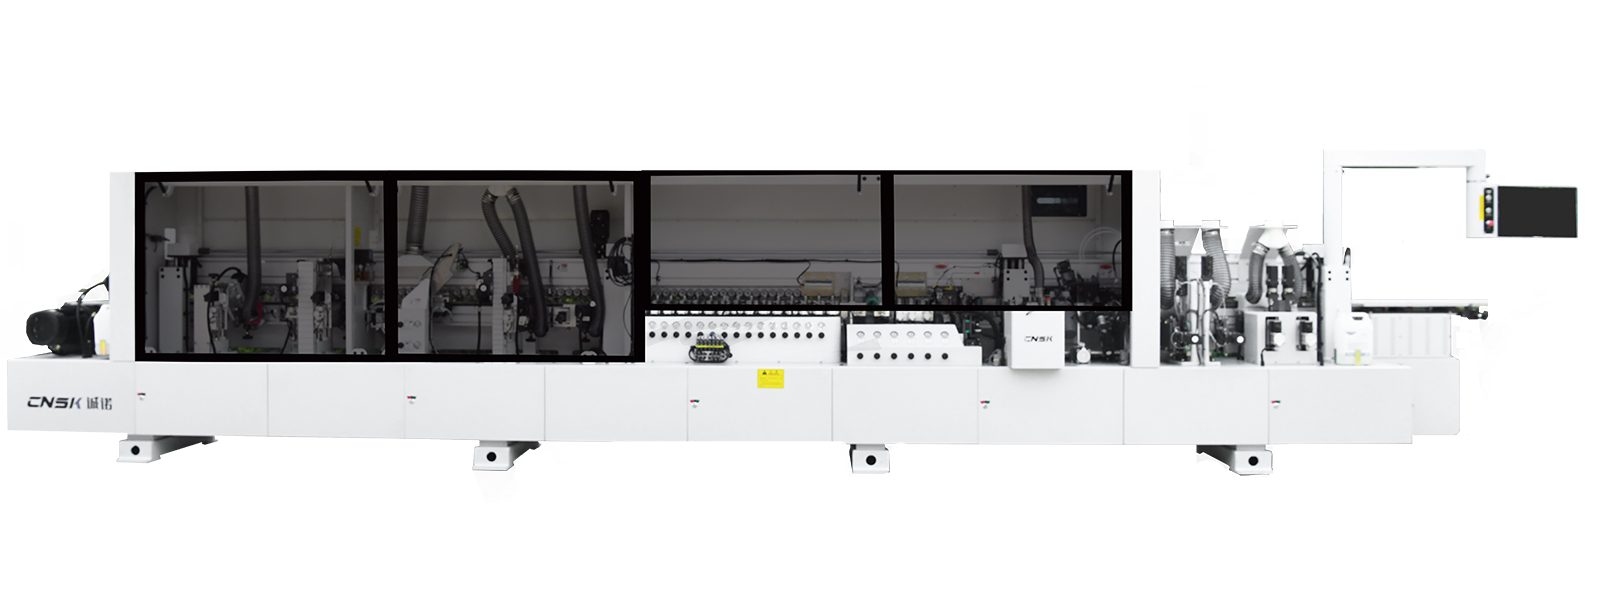
- Fourteen numbered cells: 21.5-inch industrial computer, separating agent, pre-milling, two-colour PUR no-cleaning pot, laser operating system, laser cooling system, pressing, rough and fine trimming, scraping, scraping, heavy-duty magnetic-levitation horizontal end trimming, magnetic-levitation tracking, polishing and polishing.
- The order follows the data sheet as printed: rough and fine trimming and both scraping heads sit ahead of the end trim, and the tracking head comes after it.
- Both carriages run on magnetic levitation, the end trim and the tracking head, which is the build difference against the H762.
- The laser runs from its own operating system with a closed cooling circuit, and a two-colour PUR pot is fitted for the orders that still call for adhesive.
- 9,940 mm frame, 1,040 mm wide, 1,800 mm high, 52 kW, with the feed switchable in three steps, 32, 36 and 42 m/min.
- Panels from 50 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- Rough and fine trimming on one unit, two scraping heads and two polishing stations close the sequence.
Station sequence
Station 01 is the 21.5-inch industrial computer; fourteen numbered cells run from separating agent to the second polishing station. The order follows the data sheet as printed, with the end trim at station 11 and the tracking head at station 12.
Technical data
| Model | H768 |
| Feed rate | 32 – 36 – 42 m/min |
| Panel width | ≥ 50 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 14 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 52 kW |
| Machine size (L × W × H) | 9940 × 1040 × 1800 mm |
Values from the H768 technical data sheet in the 2026 configuration list. The sheet prints the beam lift in Chinese characters; it is shown here as electric lift. The station order is reproduced as printed on the sheet.
What the machine is built to do
- Maglev on both carriagesThe end trim and the tracking head are both floated, so neither is limited by a guide rail at 42 m/min.
- Laser with a cooling circuitA closed loop holds the source at temperature, so the bond stays even across a shift.
- PUR pot on the same frameA two-colour no-cleaning pot for the orders where an adhesive is specified rather than a laser bond.
- Rough and fine on one unitBoth cuts sit on one trimming unit, so the band is not re-clamped between them.
- Two scraping heads, two polishersThe film and the trim marks come off in sequence, and two polishing pairs finish the edge.
- Lower frame than the H7621,800 mm high against 1,850 mm, on a machine that keeps the same station set and the same feed rates.
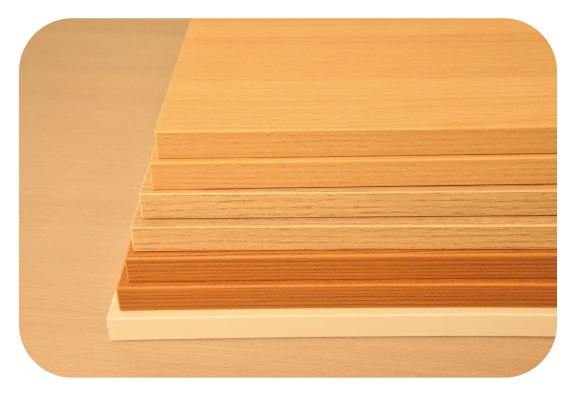
Edge samples
More from the 7 series
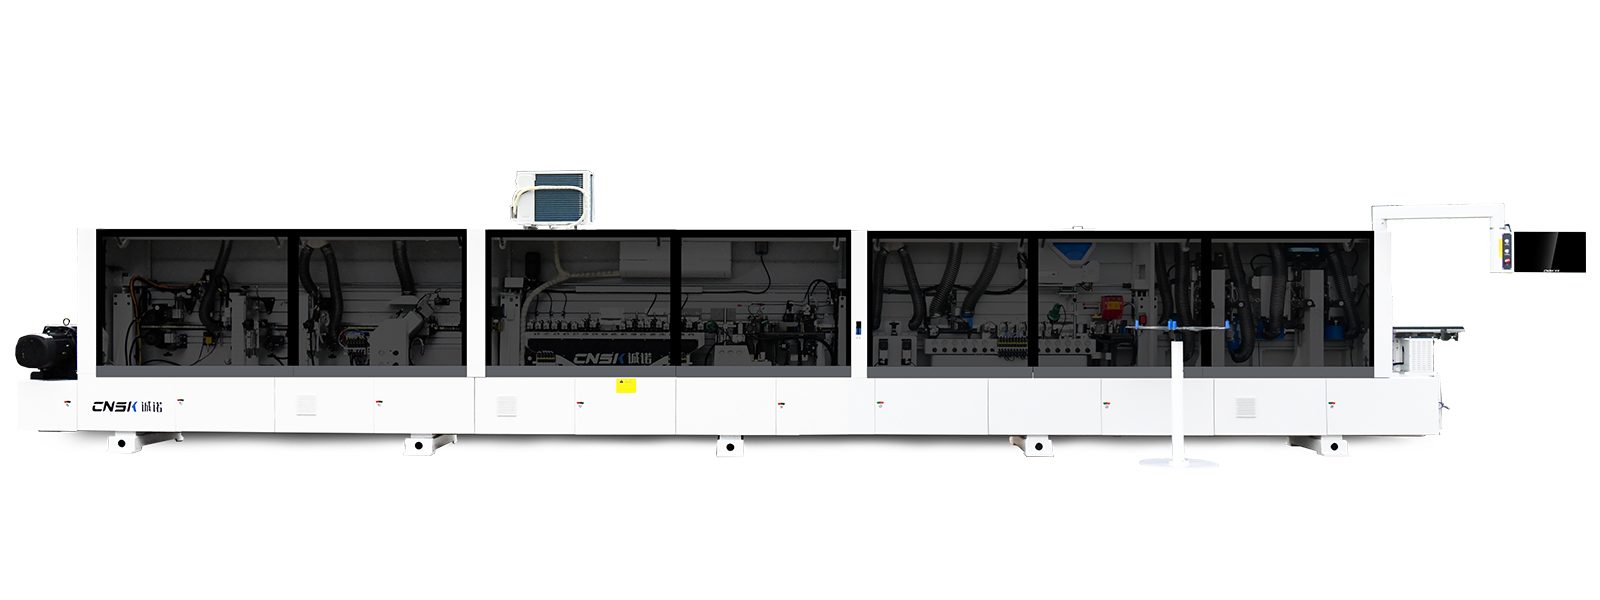
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
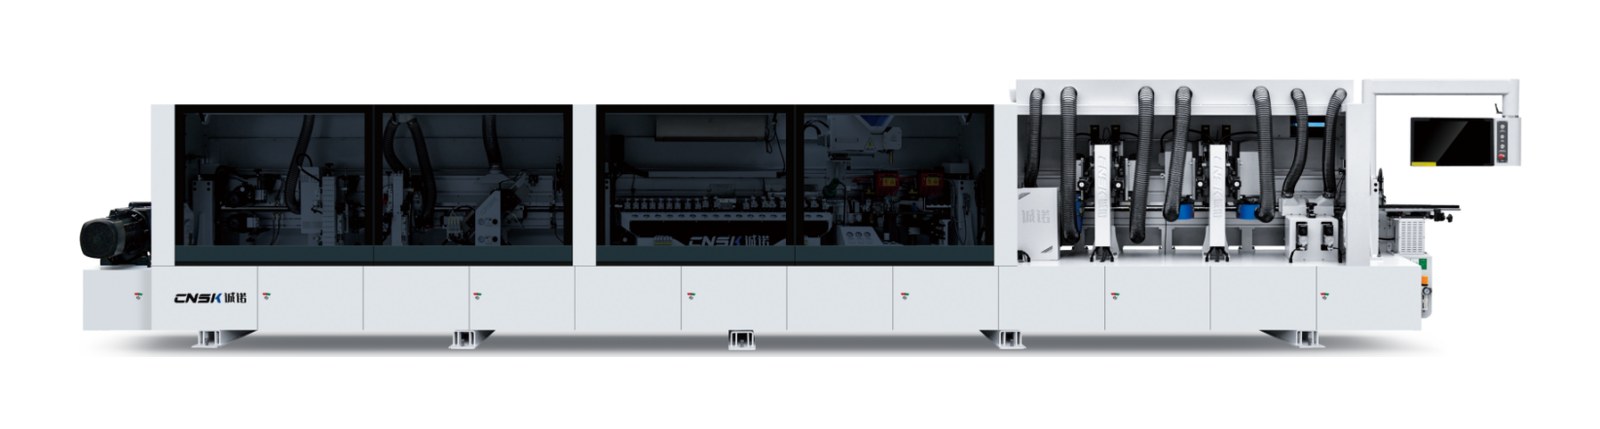
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
Five-Profile Arc and Bevel Edge Bander
Half-round, quarter-round, 45° bevel-straight, full bevel and duck-bill — five profiles on one bed.
Put H768 against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.