
45° Bevel Edge Bander
A 45° bevel line on its own bed: saw cutting, band grooving, bevel gluing and synchronous pressing, then bevel trimming and scraping — 12–40 mm panels.
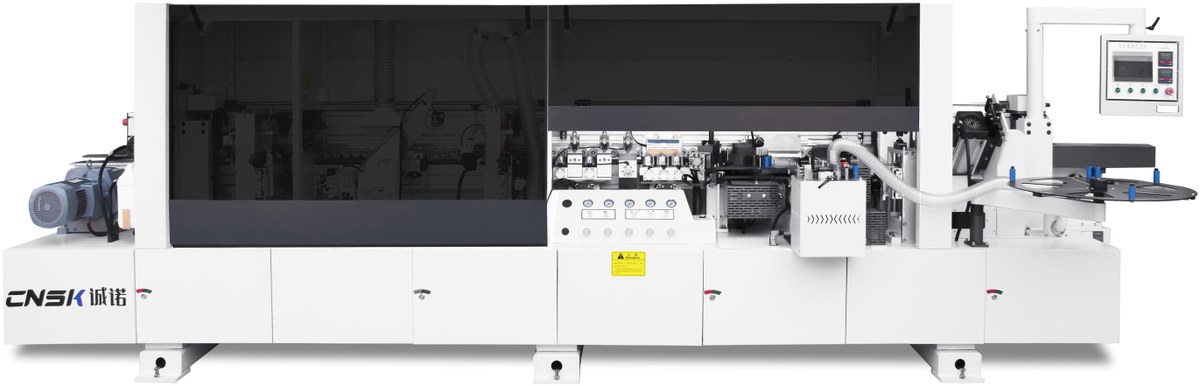
Overview
- Nine processing cells: 45° saw cutting, bevel gluing, band grooving, straight gluing, bevel and straight pressing, bevel fine trimming, end trimming, bevel scraping and polishing.
- The 45° saw cuts the square edge and mills the flat face into the bevel in the same pass, so the mitre is formed once.
- Band grooving on the inner face lets the band bend and press around the corner without tearing.
- 12–40 mm panels, ≥ 80 mm width, 14 m/min — the bevel format is a slower, more precise pass than a straight line.
- 14.5 kW total, 380 V, 0.7 MPa air.
Station sequence
Set the job on the screen; the panel then passes nine cells, bevel first and straight edge second.
Technical data
| Model | FM368C |
| Feed rate | 14 m/min |
| Panel width | ≥ 80 mm |
| Panel thickness | 12 – 40 mm |
| Edge band thickness | 0.4 – 1.5 mm |
| Edge band width | 22 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 9 |
| Control screen | Numeric panel or industrial touch screen, per configuration |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 14.5 kW |
| Machine size (L × W × H) | 5700 × 800 × 1800 mm |
Values from the 2026 configuration list; the machine size follows the configuration sheet. Confirm against the technical data sheet before the order is released.
What the machine is built to do
- 45° cut and milled in one set-upThe square edge is cut to 45° and the flat face milled into the bevel in the same pass — no second machine, no re-fixturing.
- Bevel and straight on one bedThe same line finishes the 45° mitre and the square edge; the station list changes, the operating logic does not.
- Band groovingGrooves cut on the inner face of the band let it bend and press cleanly around a 45° corner.
- Synchronous bevel pressingPressure wheels load the bevel and the straight face together, so both bonds are made in one pass.
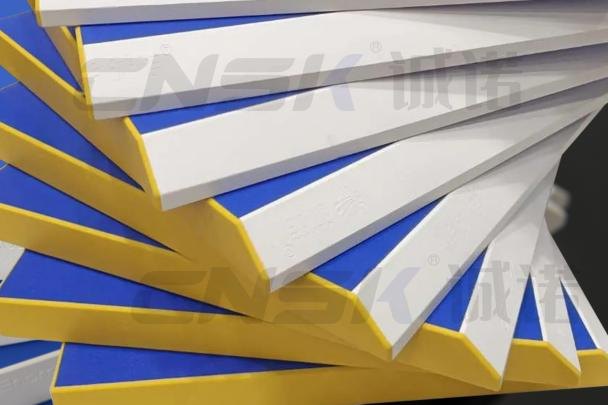
Edge samples
More from the 3 series
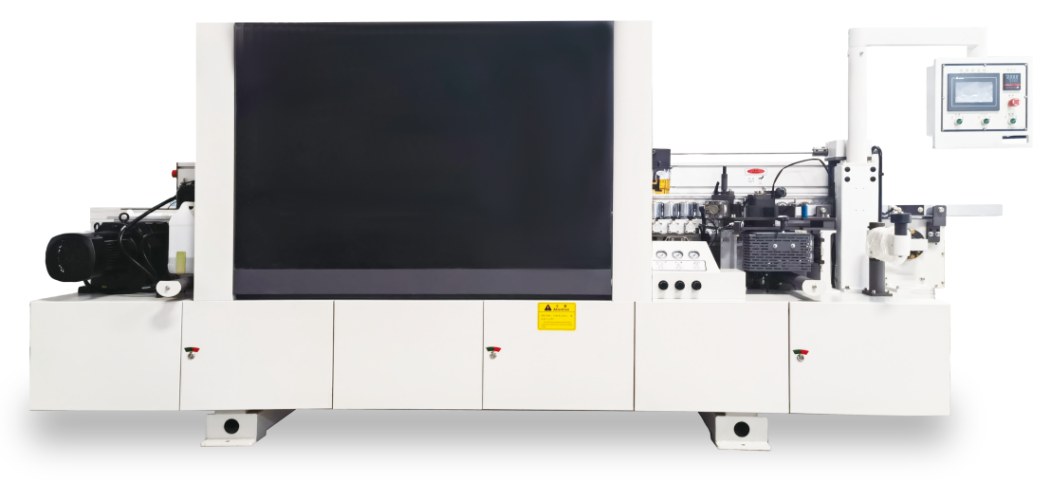
Straight Edge Bander
Seven stations on a four-metre bed: gluing, pressing, end trim, fine trim, scraping, cleaning and polishing on 9–60 mm straight panels.
Straight Edge Bander
Two glue positions and a separating-agent spray on a 5,600 mm bed.
Straight Edge Bander
Rough and fine trimming as separate heads on a 4,700 mm bed.
Put FM368C against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.