
FM368JA
Two-Pot Straight Edge Bander
Two glue pots on one line: a fast-melt tank brings the second adhesive up quickly, and a second polishing head finishes the edge after the first pass.
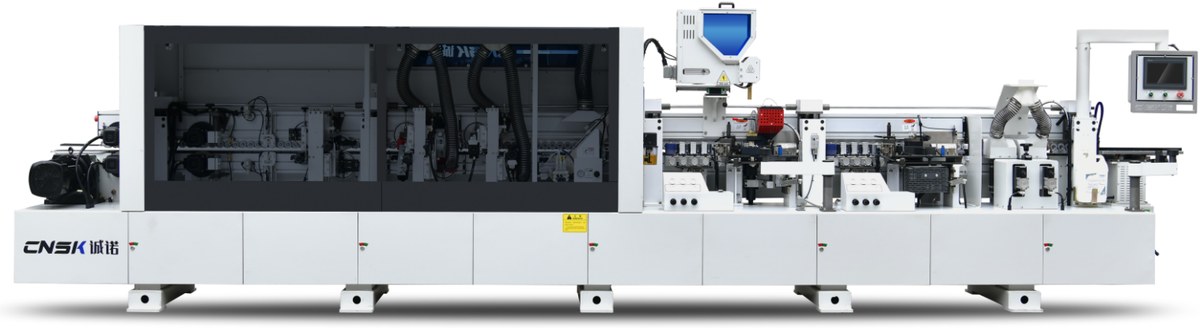
Overview
- Eleven processing cells: pre-milling, gluing, pressing, a second glue pot with fast-melt, a second pressing group, head-and-tail trimming, rough and fine trimming, scraping and double polishing.
- The two pots are switched with one key when the band or the board changes, so the line does not stop to empty and re-heat a single pot.
- Pre-milling at the head of the line, 9–60 mm panels, 16–23 m/min.
- 7,500 mm bed, for long parts and for the extra stations.
- 20 kW total, 380 V, 0.7 MPa air.
FM368JA
CNSK · Dongguan
Feed rate16 – 23 m/min
Panel thickness9 – 60 mm
Panel width≥ 50 mm
Processing stations11
Total power20 kW
Station sequence
Two glue groups: the first pot ahead of the first pressing group, the second pot with its fast-melt tank ahead of the second.
01
Control screen
Job set-up runs from the screen — parameters entered by touch or input box — and a change shows its effect at once.
02
Pre-milling
Two milling cutters re-finish the saw marks, burrs and out-of-square edges left by the panel saw, so the band seats on a clean face.
03
Gluing
Hot-melt adhesive is melted and applied to the panel edge before the band is pressed on.
04
Pressing, first group
The first pressure group seats the band applied at the first glue station.
05
Gluing furnace
EVA glue pot; the melt is held at working temperature through the shift.
06
Fast-melt glue
The fast-melt unit brings the adhesive to working temperature in less time, so a cold start does not hold up the line.
07
Pressing, second group
A second pressure group follows the second glue station, for the band applied there.
08
Head-and-tail trimming
The band is cut flush at the leading and trailing ends — quickly, and without ragged corners.
09
Rough trimming
The first trim brings the band's upper and lower edges down to the panel faces and leaves the allowance for the finishing head.
10
Fine trimming
The finishing cut takes the overhang back to the panel face; this is the pass that decides how clean the joint reads.
11
Scraping
Upper and lower edges are scraped to remove trim knife marks, and surplus glue between band and panel comes off.
12
Double polishing
Two sets of cotton wheels finish the edge, for a higher sheen on the joint than a single head gives.
Technical data
| Model | FM368JA |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 50 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 11 |
| Control screen | Numeric panel or industrial touch screen, per configuration |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 20 kW |
| Machine size (L × W × H) | 7500 × 800 × 1750 mm |
Values from the FM368JA technical data sheet and the 2026 configuration list.
What the machine is built to do
- Pre-milling before gluingTwo cutters take the saw marks and the out-of-square edge off the panel first, so the band meets a clean face instead of bridging a ripple.
- Fast-melt tankThe melt reaches working temperature in less time, so the first panel of a shift is not scrap.
- Two polishing headsA second set of cotton wheels finishes the edge after the first pass, for a higher sheen on the joint.
- Electric beam liftThe pressure beam is set from the screen rather than by hand crank, so a mixed batch of thicknesses needs no reset between panels.
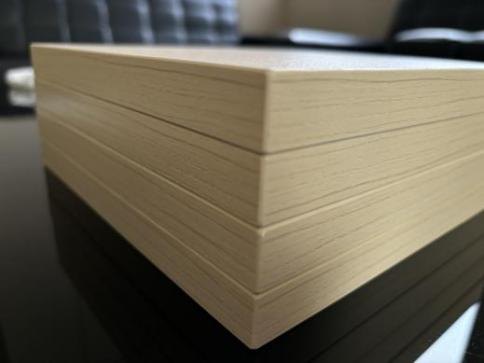
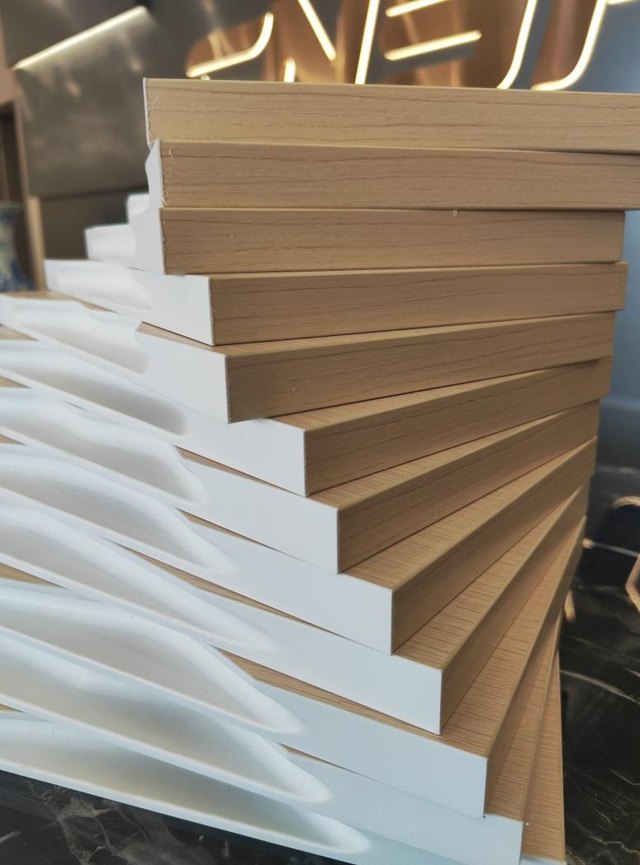
Edge samples
More from the 3 series
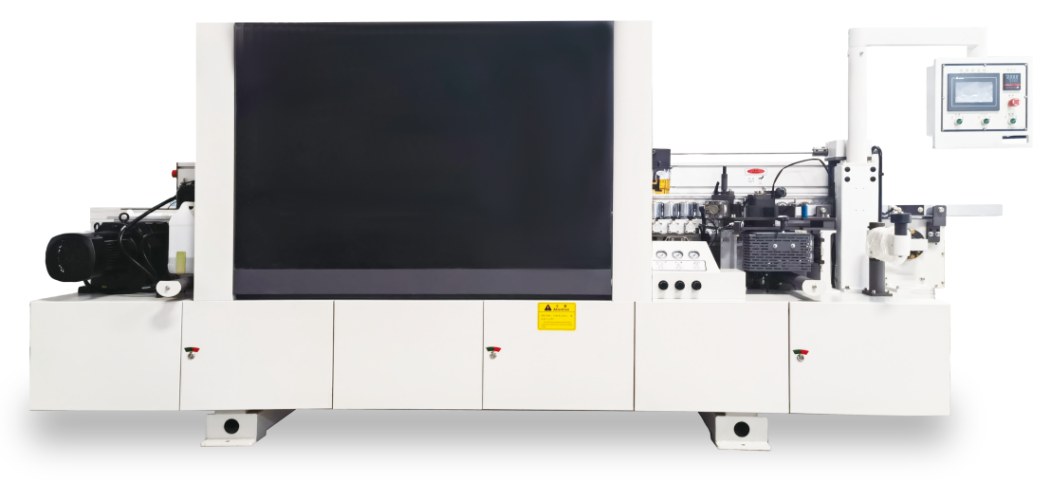
FM365
Straight Edge Bander
Seven stations on a four-metre bed: gluing, pressing, end trim, fine trim, scraping, cleaning and polishing on 9–60 mm straight panels.
7 stations9–60 mm16–23 m/min4 m bed
Read the specification
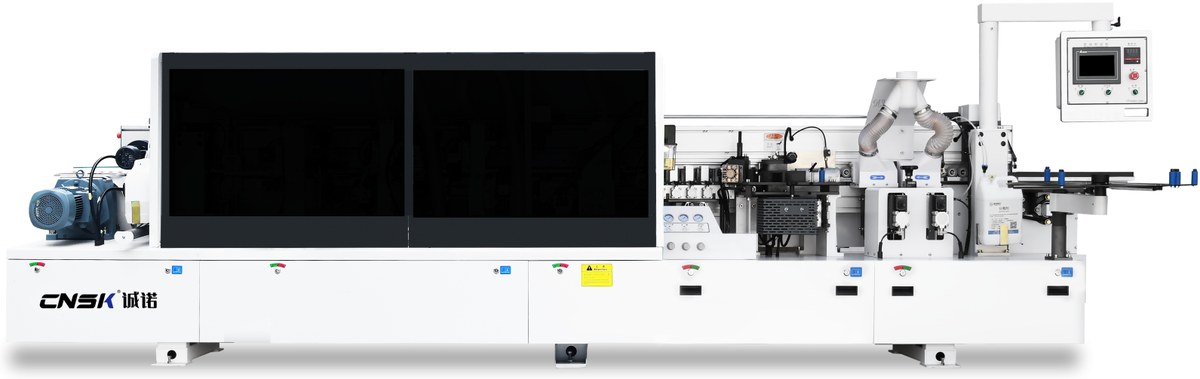
FM365J
Straight Edge Bander
Two glue positions and a separating-agent spray on a 5,600 mm bed.
9 stations9–60 mm16–23 m/min5.6 m bed
Read the specification
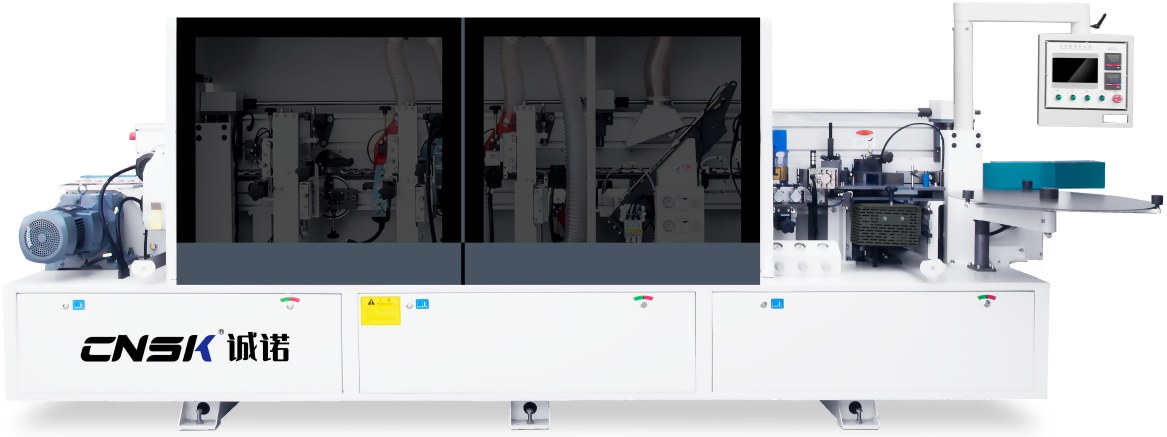
FM368
Straight Edge Bander
Rough and fine trimming as separate heads on a 4,700 mm bed.
8 stations9–60 mm16–23 m/min4.7 m bed
Read the specification
Put FM368JA against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.