
FM465J
Straight Edge Bander
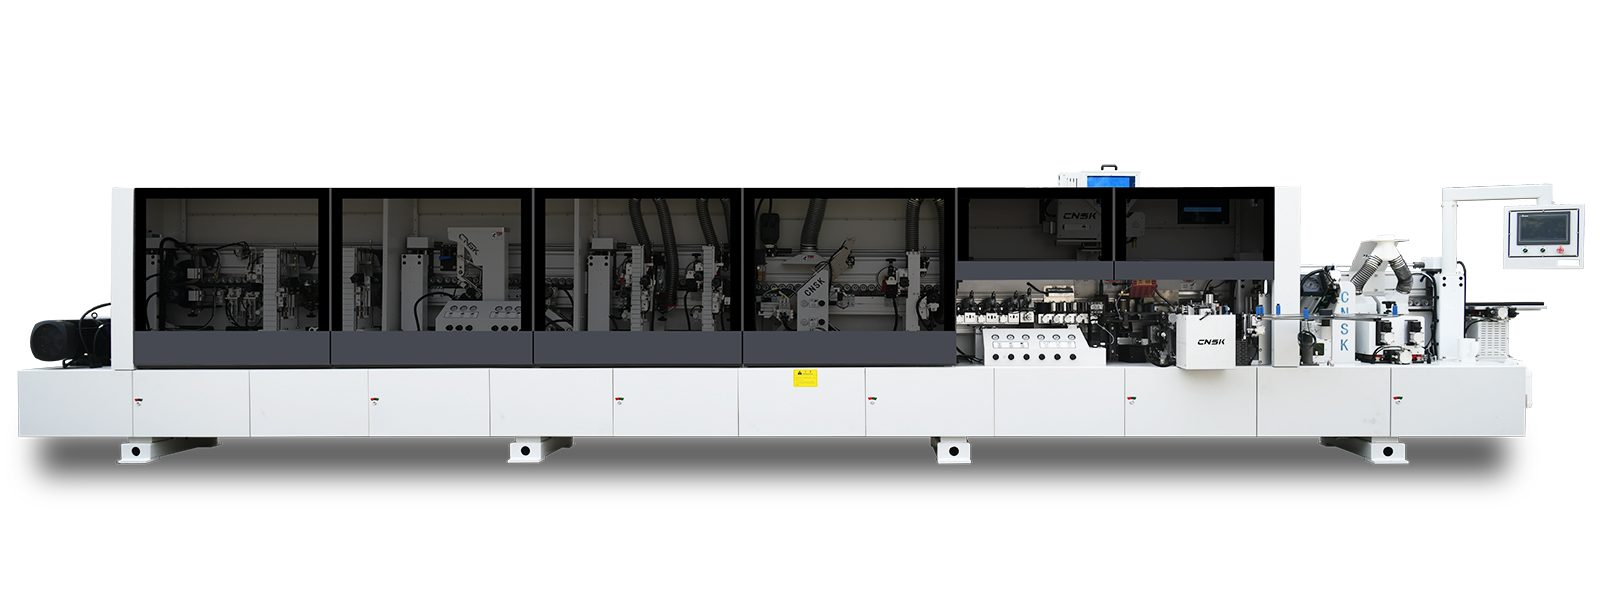
Pre-milling at the front and precise flat scraping near the end: the two stations that decide whether a glued edge reads as flat, or reads as glued.
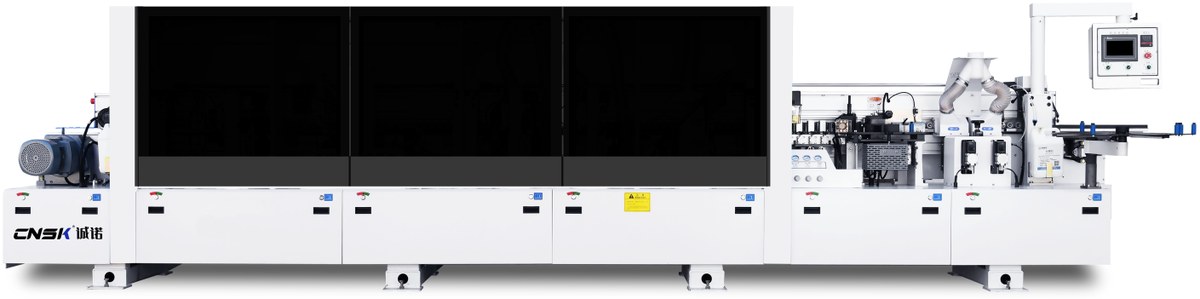
Overview
- Eleven processing stations: pre-milling, heat lamp, gluing, pressing, head and tail trimming, fine trimming, corner tracking, scraping, precise flat scraping, cleaning and double polishing.
- Pre-milling re-cuts the panel edge before gluing, so a slightly wavy saw edge still takes a straight band and a closed glue line.
- Precise flat scraping takes off the glue film left along the top and bottom of the joint, which is what shows on a lacquered or dark panel.
- 6,400 mm bed, one metre longer than the FM465, with the two extra stations that the length buys.
- 9 to 60 mm at the beam, 16 to 23 m/min feed.
- 18 kW total; frame 1,750 mm as standard, 1,350 mm for container loading.
- Specified for door panels and visible cabinet parts, where the joint is looked at rather than only measured.
FM465J
CNSK · Dongguan
Feed rate16 – 23 m/min
Panel thickness9 – 60 mm
Stations11
Bed6,400 mm
Total power18 kW
Station sequence
Screen first; pre-milling opens the sequence and double polishing closes it.
01
Control screen
Job set-up runs from the screen — parameters entered by touch or input box — and a change shows its effect at once.
02
Pre-milling
Two milling cutters re-finish the saw marks, burrs and out-of-square edges left by the panel saw, so the band seats on a clean face.
03
Heat lamp
The board and the glue are pre-heated before pressing, which keeps the bond even in cold weather.
04
Gluing
Hot-melt adhesive is melted and applied to the panel edge before the band is pressed on.
05
Pressing
High-precision pressure wheels load the band evenly as it meets the panel, so the joint sits flat and holds.
06
Head-and-tail trimming
The band is cut flush at the leading and trailing ends — quickly, and without ragged corners.
07
Fine trimming
The finishing cut takes the overhang back to the panel face; this is the pass that decides how clean the joint reads.
08
Corner rounding, head tracking
A high-frequency trimming motor profiles the corners at both ends, so the banded edge runs round the panel without a step.
09
Scraping
Upper and lower edges are scraped to remove trim knife marks, and surplus glue between band and panel comes off.
10
Precise flat scraping
A flexible scraper takes surplus hot-melt off the panel face and the band, leaving the edge flat before polishing.
11
Cleaning
Residual hot-melt is diluted and isolated before polishing, so it lifts off instead of being smeared along the edge.
12
Double polishing
Two sets of cotton wheels finish the edge, for a higher sheen on the joint than a single head gives.
Technical data
| Model | FM465J |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 50 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift, to 65 mm |
| Processing stations | 11 |
| Control screen | Control screen, per configuration |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 18 kW |
| Machine size (L × W × H) | 6400 × 800 × 1730 mm |
Values from the FM465J technical data sheet and the 2026 configuration list.
What the machine is built to do
- Eleven stations, pre-milling firstThe panel edge is milled square before the heat lamp and the glue pot, so the band meets a fresh face instead of a saw mark.
- Flat scraping before polishingGlue film along the top and bottom of the joint is scraped away, so a polished edge does not turn dull two days later.
- Two metres more bed6,400 mm against 5,300 mm on the FM465, spent on pre-milling and flat scraping rather than on more speed.
- Straight edge 9 to 60 mmSkins and worktops run on the same beam setting, entered from the screen.
- Corner trackingThe end of the panel is followed by a high-frequency motor, so the band is cut round the corner.
- 1,350 mm shipping heightThe low-frame version loads into a 40 ft container; 1,750 mm is the standard build.
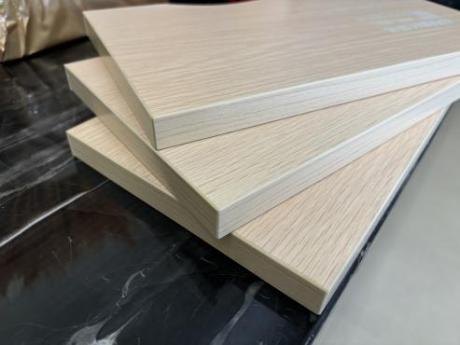
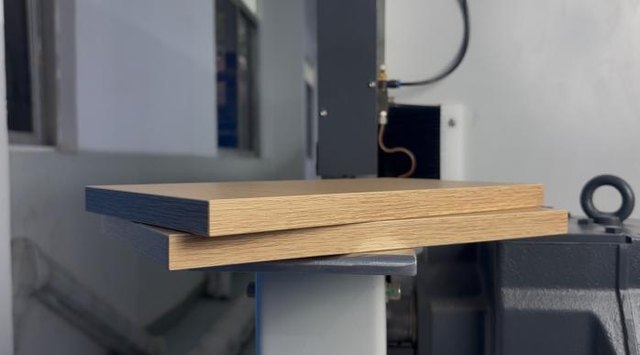
Edge samples
More from the 4 series
FM490G
Servo Narrow-Panel Edge Bander
Forty-millimetre strips, 9–60 mm thick, at 16–23 m/min — with servo control on the stations that decide the finish.
16 processing cells≥ 40 mm width9 – 60 mm thick16 – 23 m/min
Read the specification
FM468JCD
45° Bevel and Straight Edge Bander
45° bevel and straight edge banding, switched with one key, on a 9,900 mm bed.
15 processing cells8–60 / 12–40 mm45° bevelFast-melt
Read the specification
FM465
Straight Edge Bander
Nine stations on a 5,300 mm bed, 9 to 60 mm panels and no pre-milling: a straight bander for shops whose saw already cuts clean.
9 stations9–60 mm16–23 m/min5.3 m bed
Read the specification
Put FM465J against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.