
High-Speed Straight Edge Bander
Speed is the headline, but a glue line that stays closed at 26 m/min is the engineering: two baking lamps and two pressing groups hold the joint while the panel runs faster than most shops band.
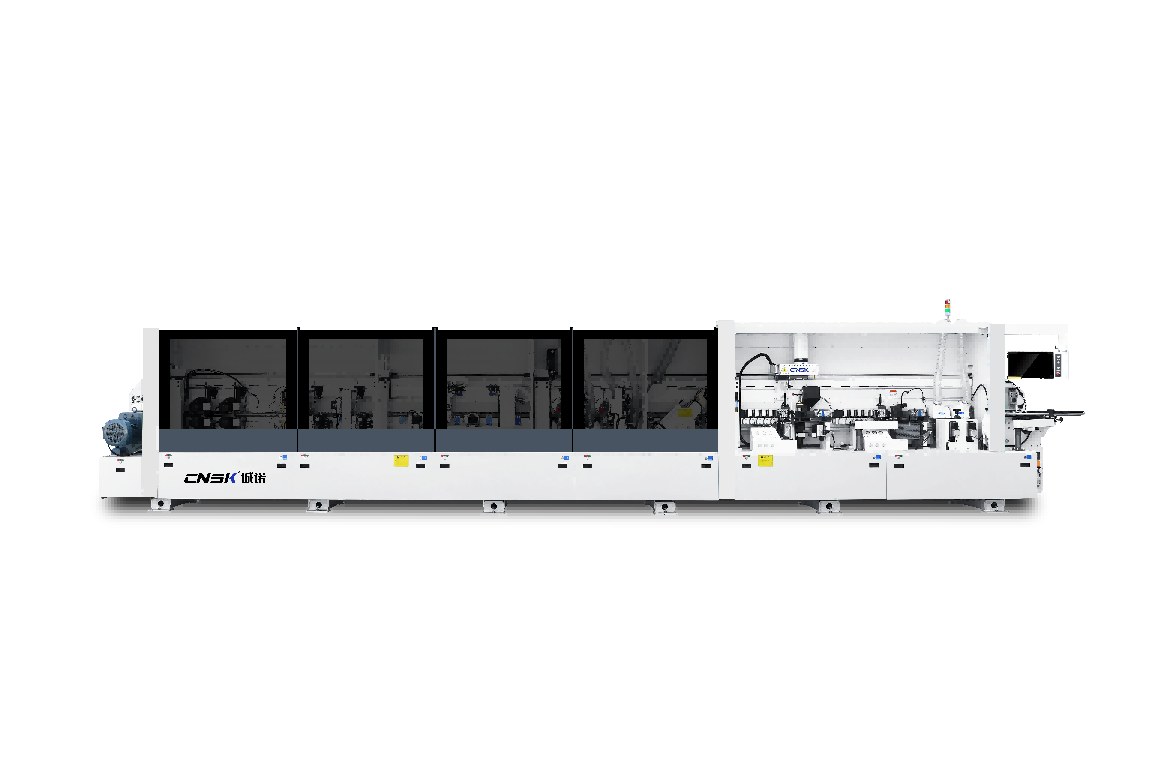
Overview
- Eighteen numbered cells: separating agent, pre-milling, baking lamp 1, straight edge gluing, pressing group 1, baking lamp 2, EVA pot, fast-melt tank, pressing group 2, double-track head-and-tail trimming, rough and fine trimming, four-head tracking, double scraping, flat scraping, cleaning, polishing 1 and polishing 2.
- 16 to 26 m/min feed. The upper end is reached with a new-generation control system and stable automatic panel feed, not by shortening the finishing train.
- Two baking lamps, one either side of the glue pot, so the panel edge is warm at the first glue station and still warm at the second.
- Two pressing groups, each following its own glue station, so a second band applied after the pot is pressed as firmly as the first.
- Double-track head-and-tail trimming, double scraping and two polishing units: the finishing end is duplicated to keep up with the feed speed.
- 9 to 60 mm panels from 60 mm wide, 0.4 to 3 mm band, 12 to 65 mm band width, 22.5 kW.
- 10,800 mm bed with a 21.5-inch industrial screen, and a 1,750 mm frame as standard.
Station sequence
Station 01 is the screen; the eighteen cells then run from separating agent to the second polishing unit.
Technical data
| Model | FM586JASK |
| Feed rate | 16 – 26 m/min |
| Panel width | ≥ 60 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 18 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 22.5 kW |
| Machine size (L × W × H) | 10800 × 800 × 1750 mm |
Values from the FM586JASK technical data sheet and the 2026 configuration list.
What the machine is built to do
- 26 m/min without a shorter trainThe feed speed is quoted with the full eighteen-cell sequence behind it, which is the only version of the number that matters on a shop floor.
- Two lamps, two pressing groupsA lamp before each glue station and a pressing group after it: the first band and the second band are heated and pressed with the same authority.
- Double-track end trimmingTwo tracks run the ends in parallel, so a pair of panels is trimmed without dropping the feed.
- Duplicated finishing endDouble scraping, precise flat scraping, cleaning and two polishing units keep the surface finish at the same standard when the line runs at 26 m/min.
- Four-head trackingTwo heads at each end cut the band round the corner radius, so a fast line still produces a corner that reads finished.
- 21.5-inch screenThe job is set on a 21.5-inch industrial computer: thickness, band and station parameters from one screen, with the option of a mouse and keyboard.
More from the 5 series
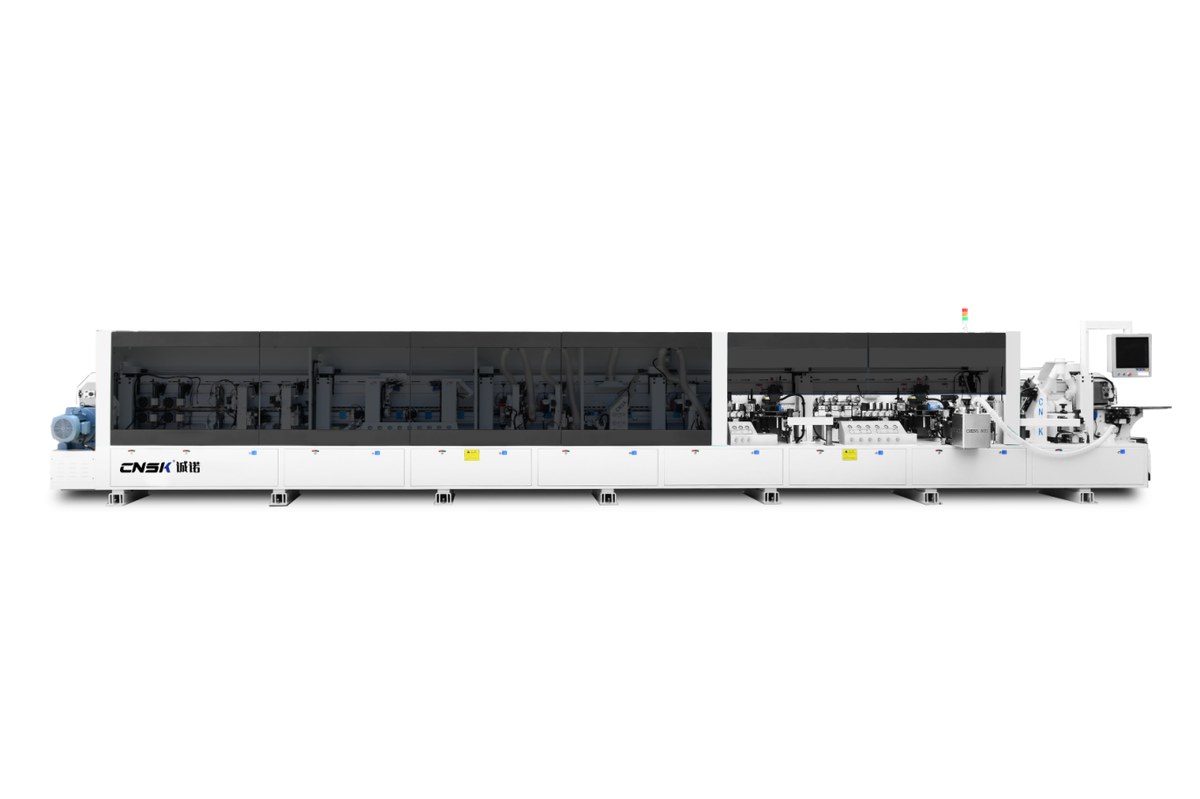
45° Bevel and Straight Edge Bander
Seventeen stations, a 45° saw and EVA plus PUR gluing on an 11.9 m bed: bevel and straight banding from one line, 9 to 60 mm.
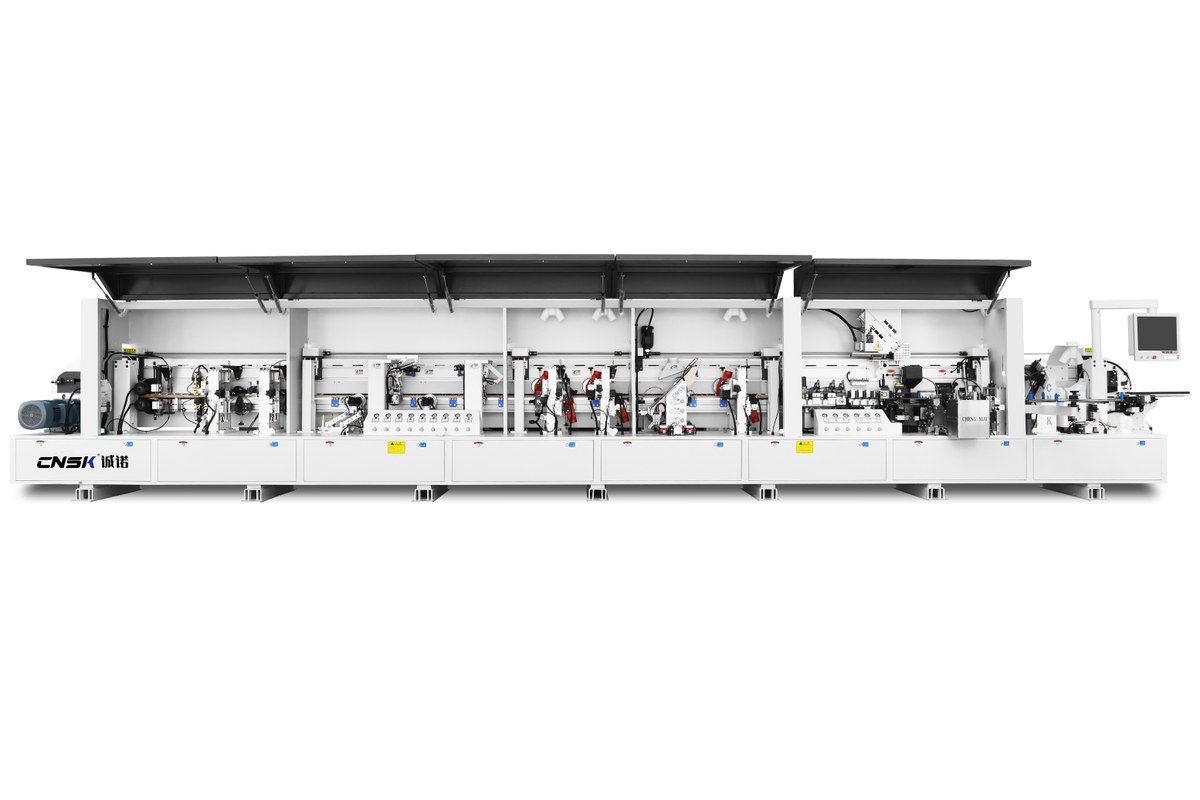
45° Bevel and Straight Edge Bander
Seventeen stations on a 10.8 m bed: 45° saw, crawler pressing and an EVA pot, banding straight and bevel edges on 9 to 60 mm.
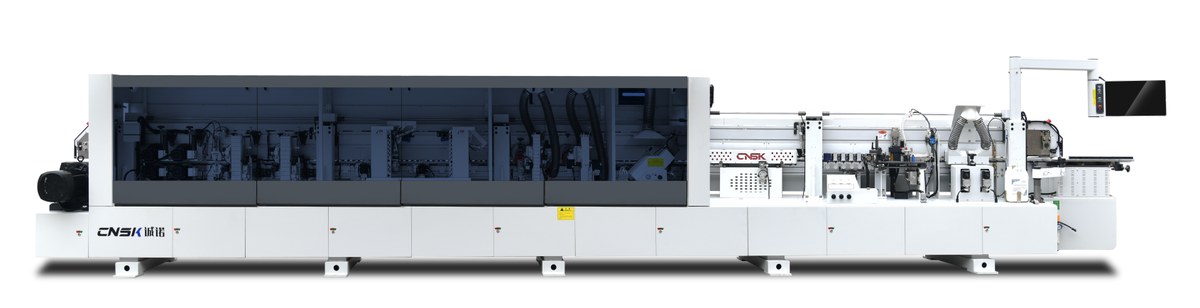
PUR Edge Bander for Honeycomb Panels
PUR banding for aluminium honeycomb and wood: fourteen stations, belt pressing and an extra-long press section, 14 to 23 m/min.
Put FM586JASK against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.