
PUR Edge Bander for Honeycomb Panels
Honeycomb and wood on one setting: the extra-long pressing section and the belt hold the skin while PUR sets, which is the part a wheel-only beam cannot do on a 10 mm aluminium skin.
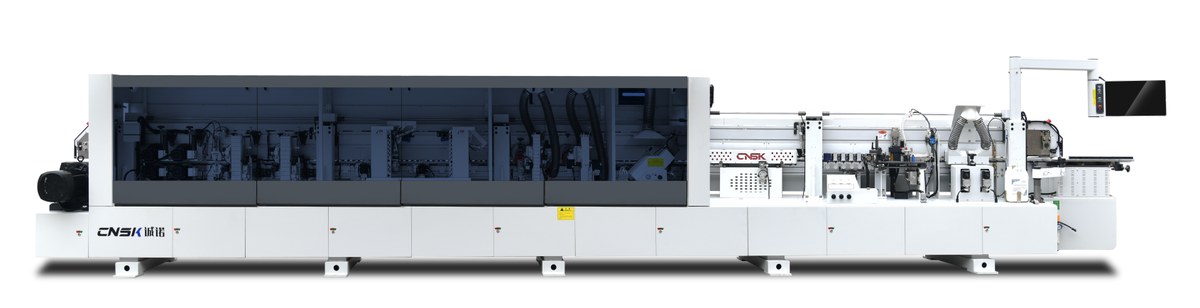
Overview
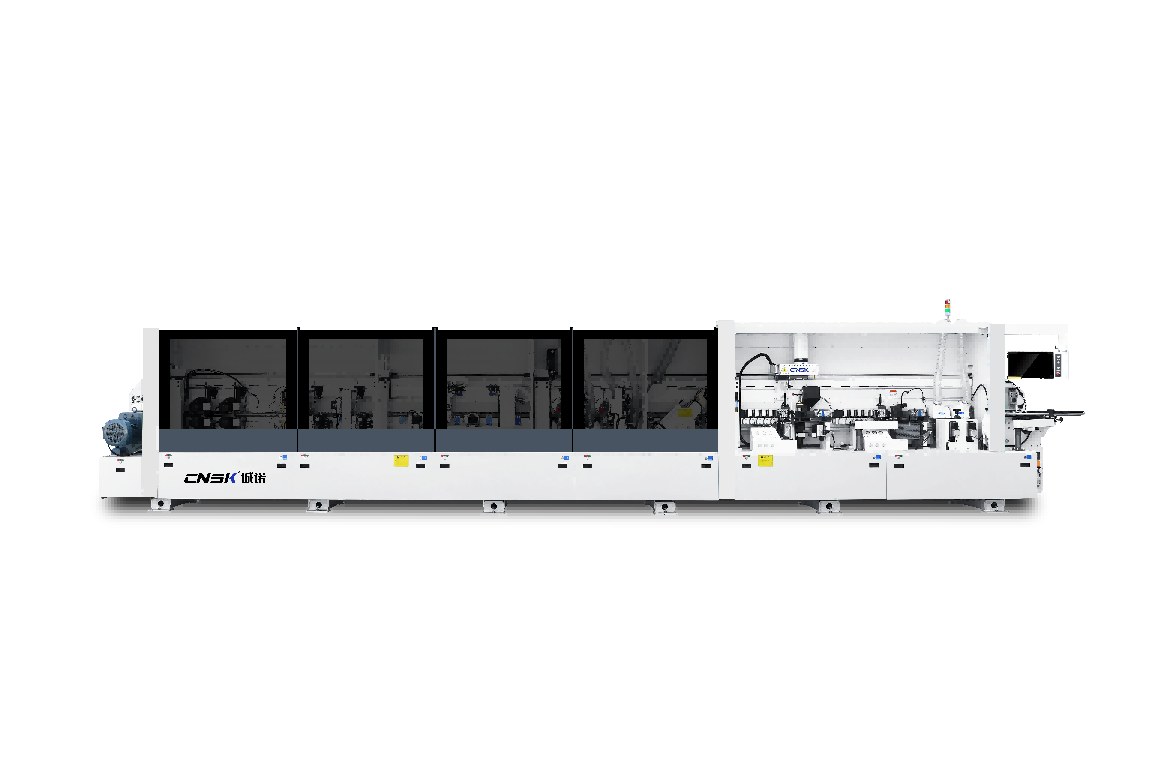
- Fourteen numbered cells behind the crawler conveyor: separating agent, pre-milling, two-colour PUR no-cleaning pot, pressing, belt pressing, double-track head-and-tail trimming, rough and fine trimming, four-head tracking, double scraping, precise flat scraping, cleaning, polishing 1 and polishing 2.
- Built for aluminium honeycomb panels: the pressing section is extra-long and a belt carries the load, so the thin aluminium skin is held flat while the adhesive cures.
- Wood and aluminium on the same machine — the edge banding of honeycomb panels and of wooden panels is switched with one key, so a mixed order does not need two lines.
- Heavy-duty frame, finish-milled on a large gantry machine, then crawler pressing: the bed stays straight under a stack of honeycomb doors.
- Two-colour PUR no-cleaning pot: two adhesive colours, even dispensing, and cleaning without a solvent soak.
- 14 to 23 m/min, 18 kW, 10,300 mm bed; band from 0.4 to 1.5 mm thick and 12 to 65 mm wide, panels from 60 mm wide and 9 to 60 mm thick.
- Four-head tracking and double scraping on the same frame, so the corner and the glue film are handled after the PUR joint.
Station sequence
Station 01 is the screen; fourteen cells follow, with the PUR pot in fourth position and the belt press behind the first pressing group.
Technical data
| Model | FM586JF |
| Feed rate | 14 – 23 m/min |
| Panel width | ≥ 60 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 1.5 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Crawler pressing, electric lift |
| Processing stations | 14 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 18 kW |
| Machine size (L × W × H) | 10300 × 900 × 1800 mm |
Values from the FM586JF technical data sheet and the 2026 configuration list. The band thickness range is narrower than on an EVA machine because the PUR pot is specified for thin aluminium and wood bands.
What the machine is built to do
- One key, aluminium or woodThe machine is specified for aluminium honeycomb as well as wooden panels, and the changeover between them is a setting rather than a rebuild.
- Belt pressing plus wheel pressingA pressure belt holds the band over a longer contact length, which is what a honeycomb panel needs; the wheel group behind it finishes the joint.
- Extra-long pressing sectionThe distance between gluing and the end of pressing is longer than on a standard line, giving PUR the time to set before the panel is trimmed.
- Gantry-milled heavy frameThe frame is machined on a large gantry mill before assembly, so the crawler stays true under load and the band does not drift on long panels.
- Two-colour PUR potTwo adhesive colours from one no-cleaning pot, dispensed evenly, with cleaning that does not need a solvent soak.
- Four-head trackingThe corner is cut round the radius at both ends, so a honeycomb door closes on a finished corner rather than a trimmed one.
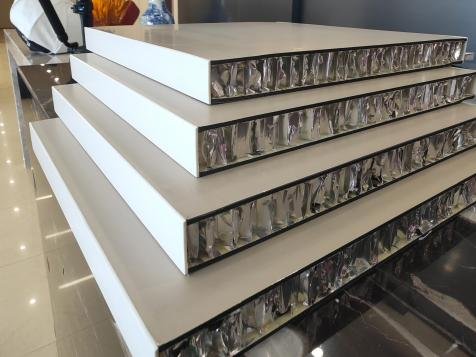
Edge samples
More from the 5 series
45° Bevel and Straight Edge Bander
Seventeen stations, a 45° saw and EVA plus PUR gluing on an 11.9 m bed: bevel and straight banding from one line, 9 to 60 mm.
45° Bevel and Straight Edge Bander
Seventeen stations on a 10.8 m bed: 45° saw, crawler pressing and an EVA pot, banding straight and bevel edges on 9 to 60 mm.
High-Speed Straight Edge Bander
Eighteen stations at 16 to 26 m/min: two lamps, two pressing groups, double end trimming, double scraping, double polishing.
Put FM586JF against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.