
Narrow-Board Edge Bander with PUR
Forty-millimetre strips are where a bander shows whether it was built for them: the FM668GJAZ carries a 1,050 mm wide bed and a heavy pressure beam, so a narrow board stays under the beam instead of tipping out of it.
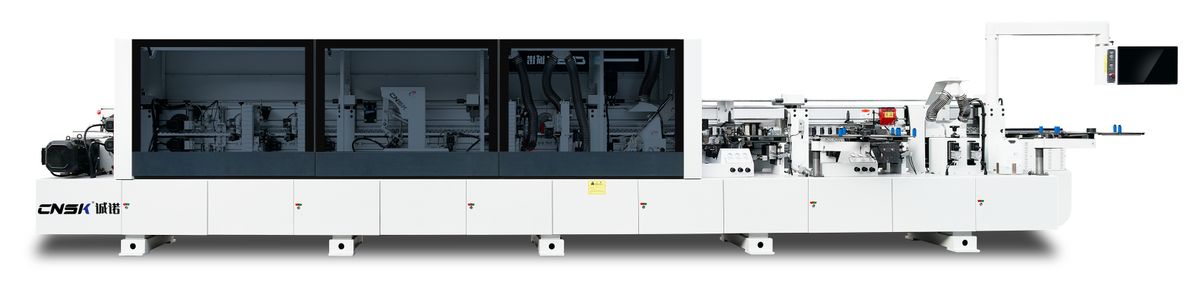
Overview
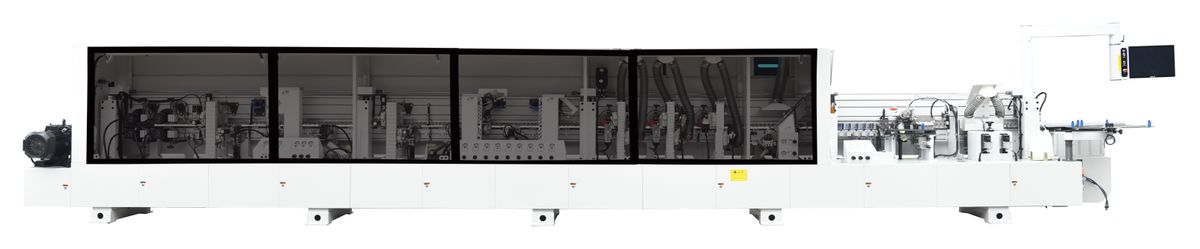
- Sixteen numbered cells behind a heavy pressure beam: separating agent, pre-milling, heat lamp 1, EVA furnace, pressing group 1, two-colour PUR pot, heat lamp 2, pressing group 2, head-and-tail trimming, rough and fine trimming, head tracking, double-edge scraping, precise flat scraping, cleaning and double polishing.
- Two heat lamps and two pressing groups, one pair either side of the two glue systems, so a band applied at the PUR pot is heated and pressed with the same authority as the one from the EVA furnace.
- 1,050 mm wide bed on a 10,080 mm frame. The extra width is frame, not decoration: it is what keeps a 40 mm strip flat when the pressure beam comes down.
- EVA furnace and a two-colour PUR no-cleaning pot on one frame, so the adhesive is picked to the order rather than to the machine.
- 16 to 23 m/min, 22 kW, panels from 40 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- Double-edge scraping and precise flat scraping finish both the straight edge and the film, and two polishing units follow them.
- 21.5-inch industrial computer as station 01, with the job set from the screen instead of from a row of dials.
Station sequence
Station 01 is the 21.5-inch screen; sixteen numbered cells run from separating agent to double polishing.
Technical data
| Model | FM668GJAZ |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Heavy-duty beam, electric lift |
| Processing stations | 16 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 22 kW |
| Machine size (L × W × H) | 10080 × 1050 × 1800 mm |
Values from the FM668GJAZ technical data sheet and the 2026 configuration list. The sheet header reads M668GJAZ; the model is FM668GJAZ.
What the machine is built to do
- Built around the 40 mm stripThe bed is 1,050 mm wide and the beam is a heavy casting: a narrow board is held across its full width, which is the difference between a flat band and one that rides up at the trimming head.
- Two lamps, two presses, two gluesHeat lamp, EVA furnace, press, PUR pot, heat lamp, press: each adhesive gets its own lamp and its own pressing group, so neither is run at the setting of the other.
- PUR without a second machineThe two-colour no-cleaning pot covers the joints that have to hold in a wet or hot room; the EVA furnace still does the everyday work.
- Head tracking at both endsThe tracking heads follow the leading and trailing end of the strip, so the band turns the corner instead of being cut square across it.
- Double scraping, then flat scrapingTwo scraping heads take the band and the glue film, and the precise flat scraper cleans the panel face behind them.
- 21.5-inch screenThickness, band and station settings are entered on a 21.5-inch industrial computer; the recipe is recalled rather than reset.
Edge samples
More from the 6 series
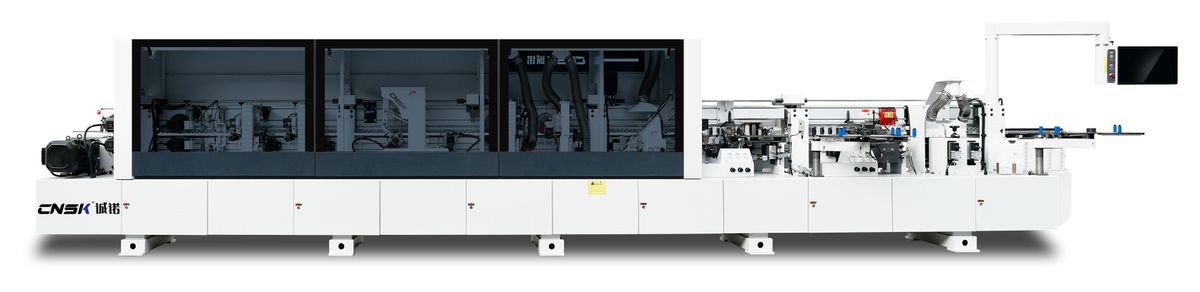
Compact Narrow-Board Edge Bander with PUR
Sixteen-station narrow-board line on a 9.3 m bed: two lamps, two pressing groups and a two-colour PUR pot, in a shorter bay.
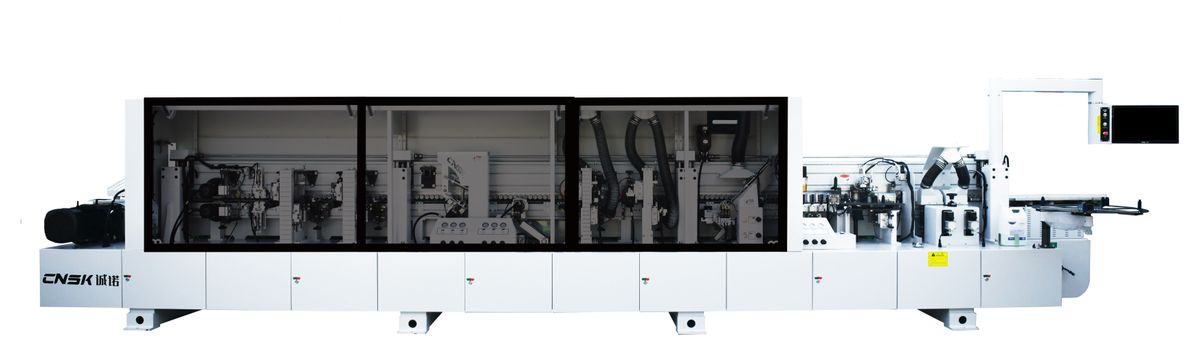
Narrow-Board Edge Bander with Grooving
Fourteen stations on a 10.1 m heavy-frame bed: band grooving, one heat lamp and press group, 18.55 kW, strips from 40 mm.
Narrow-Board Edge Bander with Diamond Trimming
Diamond fine trimming, diamond profile tracking and servo scraping on sixteen stations, for narrow boards from 40 mm wide.
Put FM668GJAZ against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.