
Compact Narrow-Board Edge Bander with PUR
Same sixteen cells as the 10.1 m machine, 760 mm shorter: the compact build of the narrow-board line for a shop where the bay, not the budget, decides.
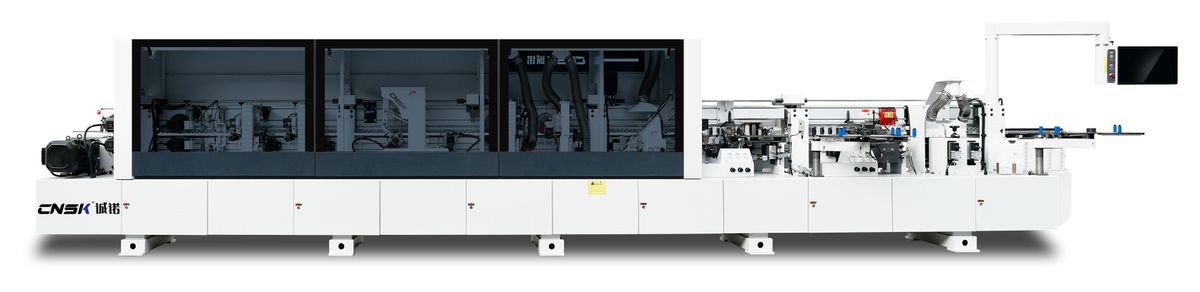
Overview
- Sixteen numbered cells: separating agent, pre-milling, heat lamp 1, EVA furnace, pressing group 1, two-colour PUR pot, heat lamp 2, pressing group 2, head-and-tail trimming, rough and fine trimming, head tracking, double-edge scraping, precise flat scraping, cleaning and double polishing.
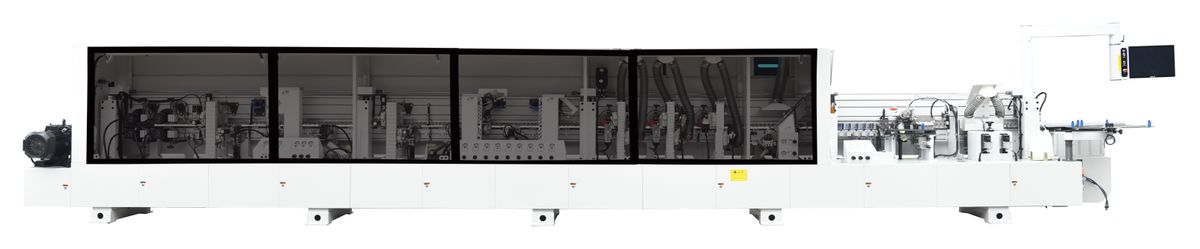
- 9,340 mm frame, 800 mm wide bed, 1,850 mm high: the same station set as the larger machine in a bay 760 mm shorter.
- Two heat lamps and two pressing groups; the EVA furnace and the PUR pot each have their own lamp and press.
- 16 to 23 m/min, 22 kW, panels from 40 mm wide and 9 to 60 mm thick.
- Double-edge scraping and precise flat scraping behind head tracking, then cleaning and two polishing units.
- The frame is annealed and the table is finish-milled, which is what keeps a 40 mm strip from drifting over a long run.
- 21.5-inch industrial computer as station 01, with the recipe recalled rather than reset.
Station sequence
Station 01 is the 21.5-inch screen; sixteen numbered cells follow, ending with double polishing.
Technical data
| Model | FM668JAZ |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 16 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 22 kW |
| Machine size (L × W × H) | 9340 × 800 × 1850 mm |
Values from the FM668JAZ technical data sheet and the 2026 configuration list.
What the machine is built to do
- Compact without dropping a stationAll sixteen cells are present; what is shorter is the bed between them, not the finishing train.
- Narrow-board geometryAn 800 mm wide bed with an annealed, finish-milled table, sized for strips from 40 mm wide rather than for a 1.2 m door.
- Two adhesives, two lamp-and-press pairsEVA furnace and two-colour PUR pot, each followed by its own heat lamp and pressing group.
- Head tracking, double scrapingThe ends are tracked before the scraping heads, so the corner is cut round the radius and the edge behind it is cleaned in the same pass.
- Annealed frameThe frame is annealed before machining to release welding stress, so the bed does not move under a long high-speed run.
- 21.5-inch screenJob data is entered on the industrial computer; band, thickness and station settings come from one screen.
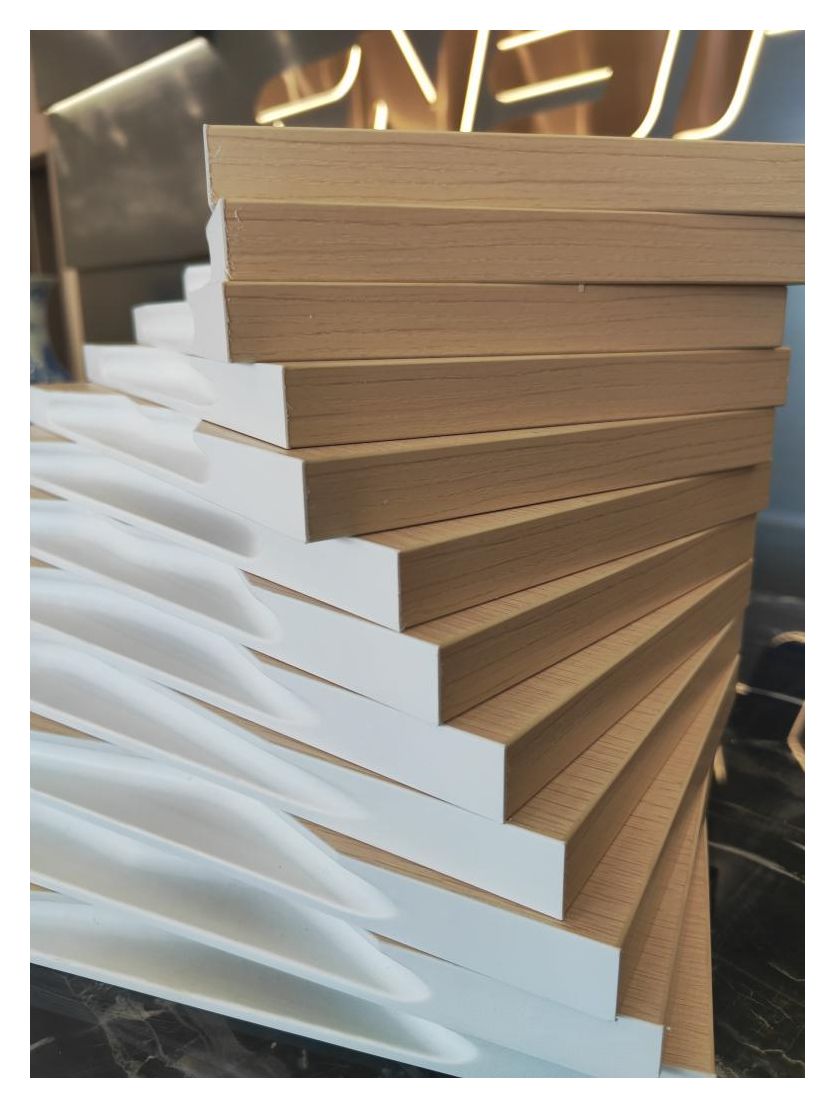
Edge samples
More from the 6 series
Narrow-Board Edge Bander with PUR
10.1 m narrow-board line: two heat lamps, two pressing groups, EVA and two-colour PUR, 40 mm strips, 16 to 23 m/min.
Narrow-Board Edge Bander with Grooving
Fourteen stations on a 10.1 m heavy-frame bed: band grooving, one heat lamp and press group, 18.55 kW, strips from 40 mm.
Narrow-Board Edge Bander with Diamond Trimming
Diamond fine trimming, diamond profile tracking and servo scraping on sixteen stations, for narrow boards from 40 mm wide.
Put FM668JAZ against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.