
Intelligent laser crawler edge banding machine
Laser bonding on a crawler bed: the functional layer on the band is activated by the laser unit at station 09, so the joint is made without a glue line and without an EVA pot in the line.
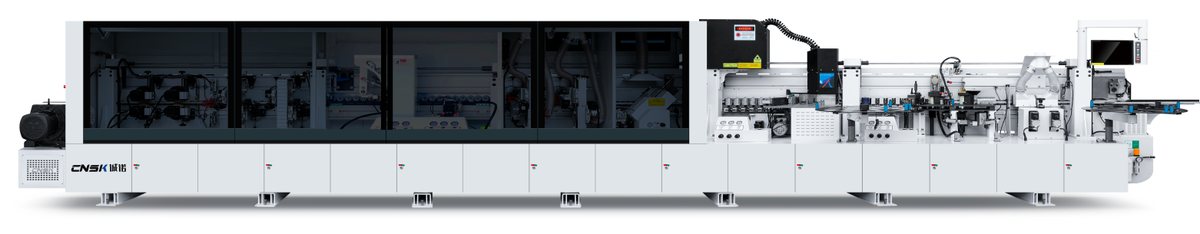
Overview
- Eighteen cells in the order printed on the sheet: 21.5-inch industrial computer, crawler conveyor, heavy-duty one-piece bed rail, separating agent, pre-milling, heat lamp, two-colour PUR pot, pressing, laser operating system, swing-type cutter and tape feed, swing-type pressing, double-track head-and-tail alignment, fine trimming, double scraping, head tracking, cleaning, polishing and notching.
- Laser bonding replaces the glue: the laser unit activates the functional layer on the band, so the finished joint has no visible glue line and needs no EVA melt in the line.
- A two-colour PUR no-cleaning pot is still fitted at station 07, so the same machine can run PUR band as well as laser band.
- Heavy-duty one-piece bed rail and a heavy steel pressure beam carry the panel; the crawler conveyor keeps the feed constant through eighteen cells.
- Panels from 60 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on a 10,300 mm frame, 950 mm wide and 1,750 mm high, with 28 kW installed.
- Notching sits last at station 18, so a slotted part comes off the line finished instead of going to a second machine.
Station sequence
Station 01 is the 21.5-inch computer, station 02 the crawler conveyor and station 09 the laser operating system; the eighteen cells follow the order printed on the sheet.
Technical data
| Model | FMK830 |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 60 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Heavy-duty electrical lift on a one-piece bed rail |
| Processing stations | 18 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 28 kW |
| Machine size (L × W × H) | 10300 × 950 × 1750 mm |
Values from the FMK830 technical data sheet in the 2026 configuration list, built to the Korean market configuration.
What the machine is built to do
- Laser unit on the frameThe laser sits between the pressing groups and activates the band's functional layer, which is what removes the glue line from the joint.
- Two-colour PUR as wellThe pot switches between two PUR colours without a solvent flush, so laser and PUR work can be quoted from the same machine.
- Swing cutter and swing pressThe cutter swings to the band angle and the pressure roller follows it on an arc, which cushions the load at the joint.
- Double-track end trimmingTwo tracks move the end heads, so both ends are aligned and cut without dropping the feed speed.
- Heavy bed railA one-piece guide rail and a heavy pressure beam hold the panel flat under the laser head.
- Notching on the same lineThe slotting unit at station 18 cuts the notches a profile part needs after banding.
More from the FMK series
Intelligent PUR track edge banding machine
Reverse-layout PUR line, eighteen cells: two PUR pots with heat lamps, unpowered trimming and head tracking, 16 to 26 m/min at 28 kW.
HeavyDuty Laser TrackType Edge Banding Machine
Twenty cells on a synchronous track: two EVA furnaces, laser unit, servo trims and chamfer tracking, 36 kW.
High Pressure Beam Track Type Edge Bander
Twenty-one cells on a high-pressure beam track: electric glue pot, two heated presses, servo trims, 28.95 kW.
Put FMK830 against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.