
HeavyDuty Laser TrackType Edge Banding Machine
Two independent EVA furnaces on the upper frame, each able to hold a different colour, and a laser unit further down the same bed: colour changes and glue-free work run on one machine.
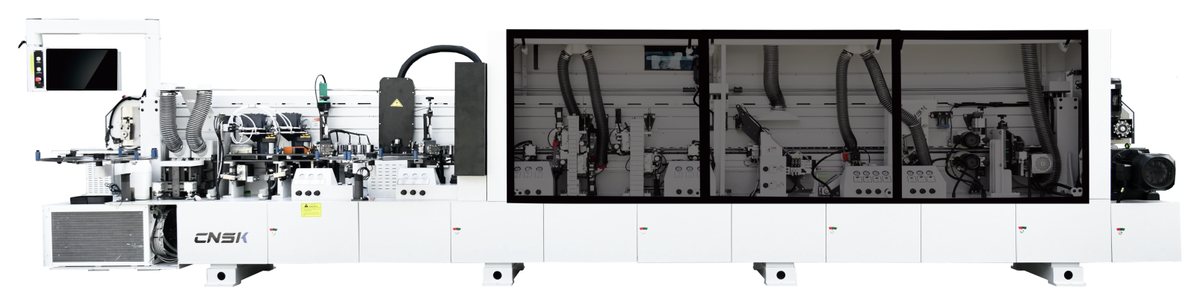
Overview
- Twenty cells in the order printed on the sheet: synchronous caterpillar conveyor, heavy-duty one-piece bed rail, wide screen, separating agent, pre-milling, heat lamp, dual pneumatic upper glue pot, heated pressing, laser operating system, swing-type pressing, unpowered tail trimming, servo fine trimming, servo scraping, unpowered end trimming, head-and-tail trimming for narrow boards, double-end chamfer tracking, cleaning, polishing, horizontal and vertical grooving and the track synchronous motor.
- Two EVA furnaces on the upper frame, each able to hold a different colour, so a colour change is a switch rather than an empty-and-refill.
- A laser operating system at station 09 bonds the functional layer of the band without a glue line, on the same bed as the EVA pots.
- Panels from 60 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on a 7,980 mm frame, 950 mm wide and 1,900 mm high, with 36 kW installed and a body weight of 3,600 kg.
- Heated pressing follows the first pot, so the band and the glue are warm when the pressure goes on.
- Servo fine trimming and servo scraping are positioned from the screen; the chamfer tracking unit then cuts both ends of the band at the corner.
Station sequence
Station 01 is the synchronous caterpillar conveyor and station 02 the bed rail; the twenty cells follow the order printed on the sheet, with the two EVA furnaces at station 07 and the laser unit at station 09.
Technical data
| Model | FMK850MS |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 60 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Heavy-duty electrical lift, one-piece bed rail |
| Processing stations | 20 |
| Control screen | High-definition wide screen |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 36 kW |
| Machine size (L × W × H) | 7980 × 950 × 1900 mm |
Values from the FMK850MS technical data sheet in the 2026 configuration list. The machine name is printed there as HeavyDuty Laser TrackType Edge Banding Machine; the page keeps it as written and adds the body weight of 3,600 kg from the same sheet.
What the machine is built to do
- Two colours without stoppingTwo furnaces hold two EVA colours; changing colour is a station setting, not a pot that has to be emptied and cleaned.
- Laser on the same bedThe laser unit gives a glue-free joint for high-gloss work, while the EVA pots cover the volume.
- Heavy rail and synchronous trackA one-piece guide rail and a synchronous track motor keep the panel locked to the station timing at 36 kW of installed load.
- Servo trimming and scrapingBoth heads are positioned by servo, so a band change is a screen value rather than a manual reset.
- Built for narrow boardsStations 15 and 16 are the narrow-board end trimming and the double-end chamfer tracking, which is where a 60 mm part is decided.
- Grooving at the endA horizontal and vertical grooving unit at station 19 lets the same line produce groove profiles.
More from the FMK series
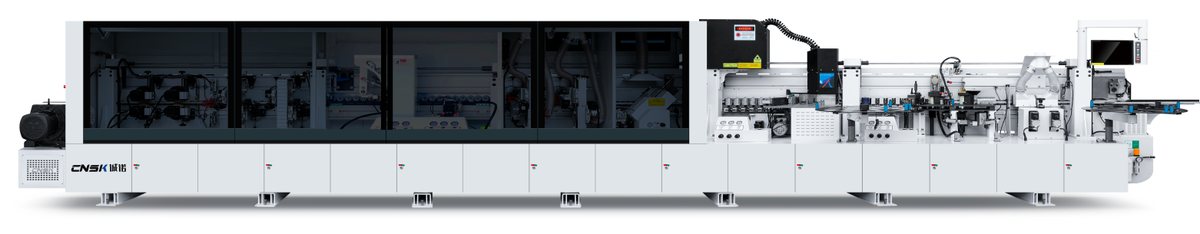
Intelligent laser crawler edge banding machine
Eighteen cells on a 10.3 m crawler bed: two-colour PUR pot, laser bonding, swing cutter and notching, 28 kW.
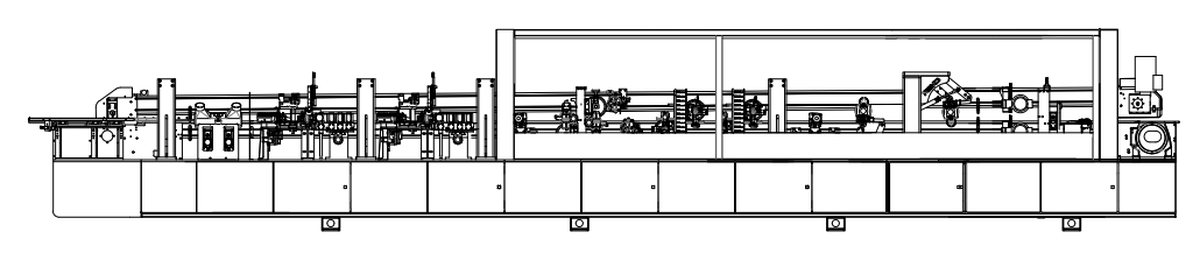
Intelligent PUR track edge banding machine
Reverse-layout PUR line, eighteen cells: two PUR pots with heat lamps, unpowered trimming and head tracking, 16 to 26 m/min at 28 kW.
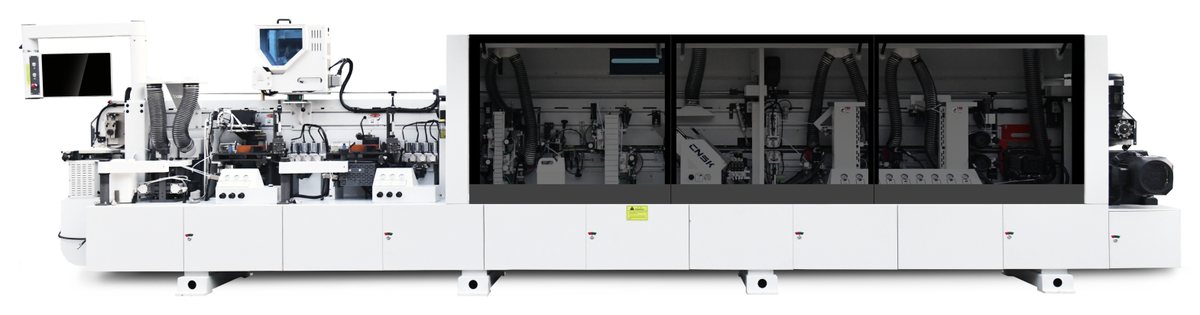
High Pressure Beam Track Type Edge Bander
Twenty-one cells on a high-pressure beam track: electric glue pot, two heated presses, servo trims, 28.95 kW.
Put FMK850MS against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.