
Intelligent laser edge banding machine
Three ways to bond on one frame: an EVA furnace, a two-colour PUR pot and a laser unit, so the machine can be quoted against whatever band the job specifies.
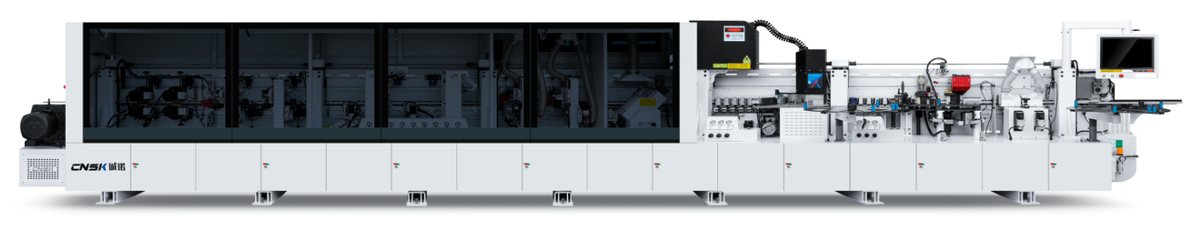
Overview
- Sixteen cells in the order printed on the sheet: 21.5-inch industrial computer, separating agent, pre-milling, gluing furnace, two-colour PUR pot, pressing, laser operating system, laser cooling system, pressing, head-and-tail trimming, rough and fine trimming, four-head tracking, double scraping, precise flat scraping, polishing head 1 and polishing head 2.
- An EVA gluing furnace and a two-colour PUR pot sit ahead of the laser unit, so EVA, PUR and laser band all run on the same bed.
- The laser unit is followed by its own cooling system, which keeps the head at working temperature through a shift.
- Panels from 40 mm wide and 9 to 60 mm thick, band 0.4 to 3 mm thick and 12 to 65 mm wide.
- 16 to 23 m/min on a 10,060 mm frame, 850 mm wide and 1,830 mm high, with 22.5 kW installed.
- Pressing runs before and after the laser, so the band is seated, activated and pressed again.
- Double scraping takes the trim marks off both edges, then precise flat scraping and two polishing heads finish the joint.
Station sequence
Station 01 is the 21.5-inch computer, station 04 the EVA gluing furnace and station 07 the laser operating system; the sixteen cells follow the order printed on the sheet.
Technical data
| Model | Laser830 |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 16 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 22.5 kW |
| Machine size (L × W × H) | 10060 × 850 × 1830 mm |
Values from the Laser830 technical data sheet in the 2026 configuration list. The sheet prints the model as Laser830; the 45° build is a separate document and a separate page.
What the machine is built to do
- EVA, PUR and laser on one bedThree bonding paths in one station list: the machine is specified against the band, not the other way round.
- Cooling behind the laserA dedicated cooling system follows the laser unit, which is what a continuous run needs.
- Two polishing headsThe joint is finished twice, which is where a laser band reads against a lacquered panel.
- Double scrapingBoth edges of the band are scraped, so trim marks do not survive into the polish.
- Four-head trackingFour motors carry the tracking head and turn both corners.
- Eighteen-thirty height850 mm wide, 1,830 mm high: the bed is narrow enough for a single bay and tall enough for the tracking unit.
More from the 8 series
Skeleton-Line Grille Edge Bander
Skeleton-line doors, grille slats and standard straight edge banding on one track-fed 13-metre bed.
Intelligent laser edge banding machine
Fourteen cells on a 10.1 m frame: two-colour PUR pot, laser unit with cooling, four-head tracking and double polishing, at 22.5 kW.
Intelligent laser edge banding machine
Twenty-four cells with a 45 degree saw, bevel and straight gluing, laser unit and bevel face trimming, 32 kW.
Put Laser830 against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.