
Narrow-Board Edge Bander with Diamond Trimming
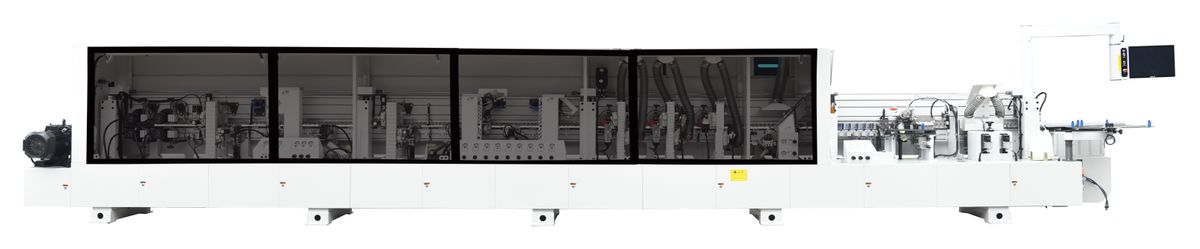
Diamond cutters and servo scraping are what a shop buys when the edge has to look finished under a lacquer: the FM669GD puts both on a narrow-board line, with a two-colour PUR pot between them.
Overview
- Sixteen numbered cells: separating agent, pre-milling, heat lamp, two-colour PUR pot, pressing, head-and-tail trimming, rough and fine trimming, diamond fine trimming, four-head profile tracking, servo double scraping, diamond profile tracking, servo diamond scraping, flexible flat scraping, cleaning and double polishing.
- Diamond fine trimming takes a shear cut instead of a crush cut, which is the difference between an edge that photographs clean and one that shows a faint line.
- Two tracking units and two scraping units: a profile tracker and a servo double scraper, then a diamond profile tracker and a servo diamond scraper, each following its own cutter.
- Servo on the scraping heads rather than a pneumatic stop: the scraper follows the band contour, so a 0.4 mm band and a 3 mm band are both taken clean.
- 8,990 mm frame, 16 to 23 m/min, 19.5 kW, panels from 40 mm wide and 9 to 60 mm thick.
- Two-colour PUR no-cleaning pot as the only glue system, which is a deliberate choice: a line this far into finishing is usually run on PUR work.
- Flexible flat scraping, cleaning and double polishing after the diamond cutters.
Station sequence
Station 01 is the 21.5-inch screen; the diamond and servo finishing cells sit from ninth position onward.
Technical data
| Model | FM669GD |
| Feed rate | 16 – 23 m/min |
| Panel width | ≥ 40 mm |
| Panel thickness | 9 – 60 mm |
| Edge band thickness | 0.4 – 3 mm |
| Edge band width | 12 – 65 mm |
| Pressure beam | Electric lift |
| Processing stations | 16 |
| Control screen | 21.5-inch industrial computer |
| Input voltage | 380 V |
| Air pressure | 0.7 MPa |
| Total power | 19.5 kW |
| Machine size (L × W × H) | 8990 × 800 × 1900 mm |
Values from the FM669GD technical data sheet and the 2026 configuration list. The sheet names the trimming cells diamond fine trimming and diamond edge scraping; the drive on the scraping heads is servo.
What the machine is built to do
- Diamond fine trimmingDiamond cutters shear the band instead of crushing it, so the joint keeps its colour and does not show a pale line after lacquering.
- Two cutters, two trackersA four-head profile tracker follows the first cut and a diamond profile tracker follows the second, each with its own scraper behind it.
- Servo scrapingThe scraping heads are driven rather than sprung, so they follow the contour of the band on both thin and thick stock.
- PUR only, on purposeA two-colour no-cleaning pot, for shops whose work has to hold in heat or moisture; there is no EVA furnace on this specification.
- Narrow-board bed8,990 mm frame with an annealed body and a finish-milled table, sized for strips from 40 mm wide.
- 21.5-inch screenSixteen station parameters on one industrial screen, recalled as a recipe.
More from the 6 series
Narrow-Board Edge Bander with PUR
10.1 m narrow-board line: two heat lamps, two pressing groups, EVA and two-colour PUR, 40 mm strips, 16 to 23 m/min.
Compact Narrow-Board Edge Bander with PUR
Sixteen-station narrow-board line on a 9.3 m bed: two lamps, two pressing groups and a two-colour PUR pot, in a shorter bay.
Narrow-Board Edge Bander with Grooving
Fourteen stations on a 10.1 m heavy-frame bed: band grooving, one heat lamp and press group, 18.55 kW, strips from 40 mm.
Put FM669GD against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.